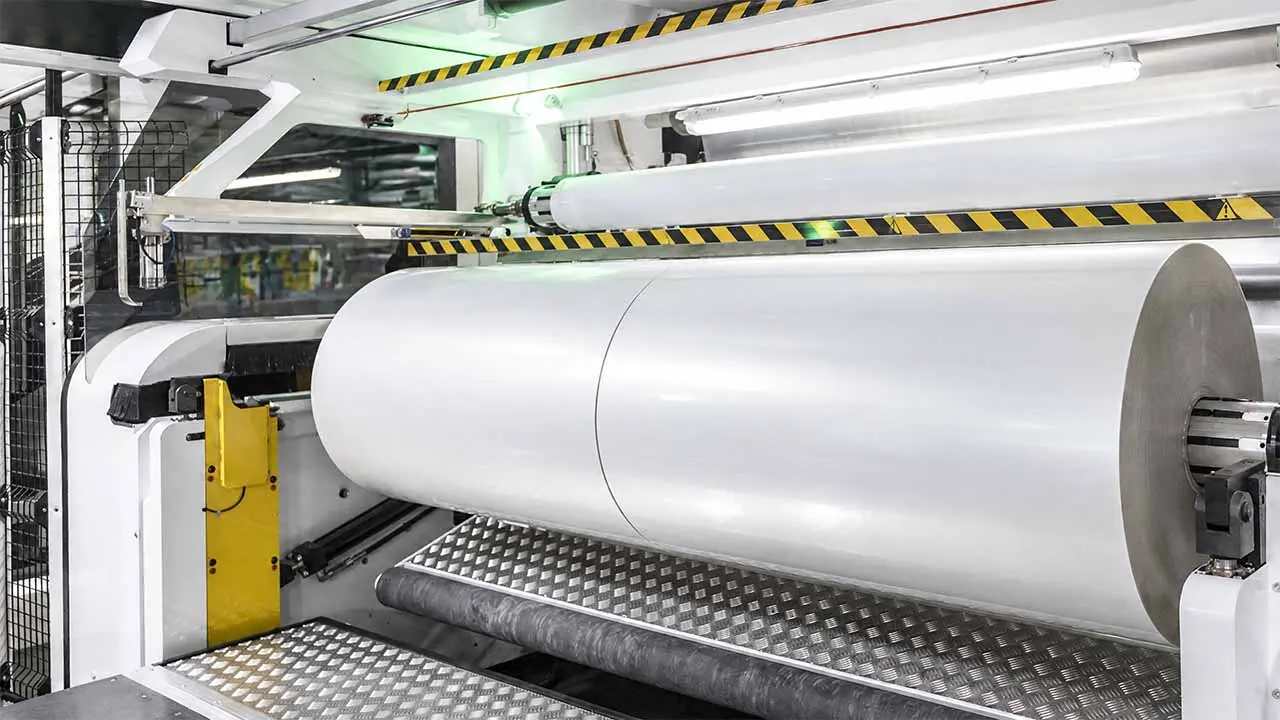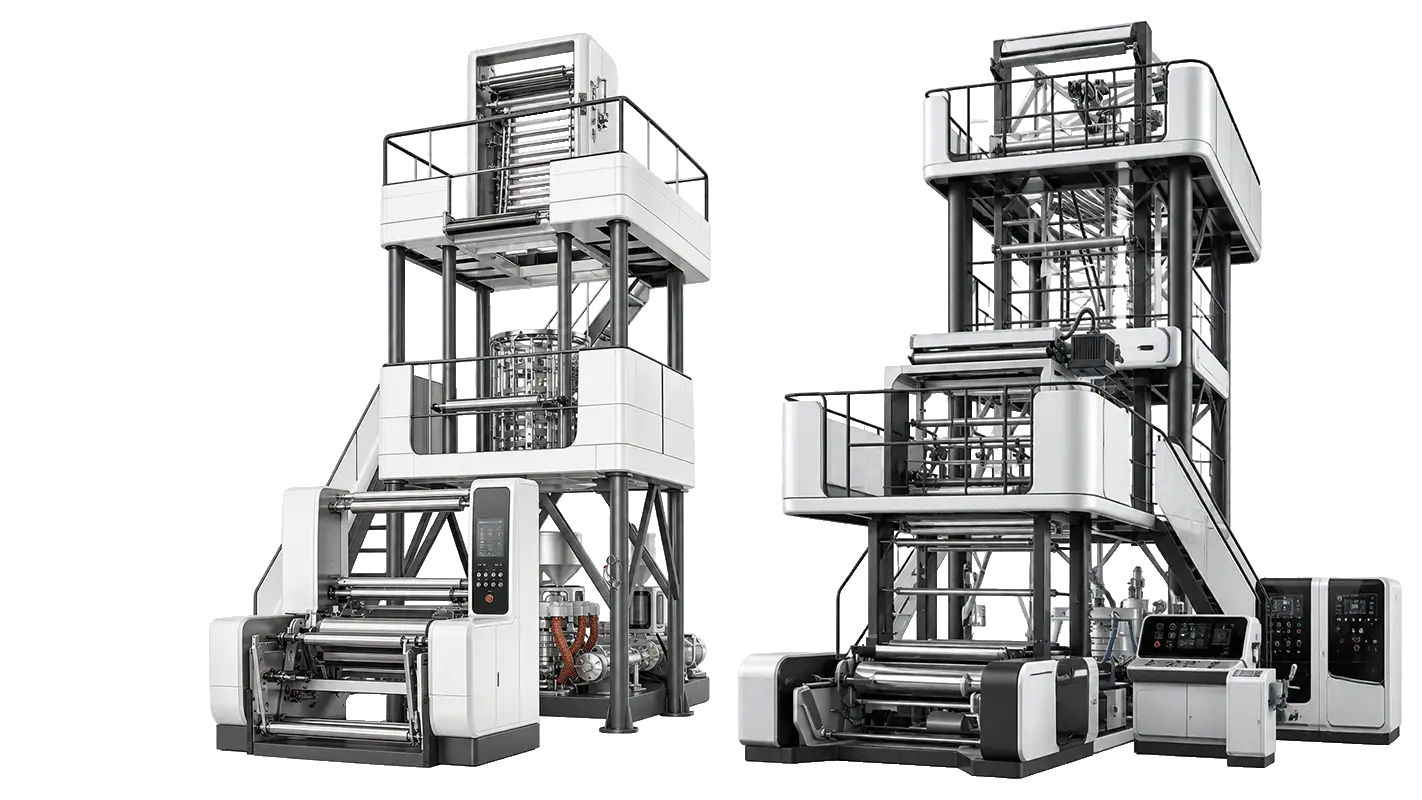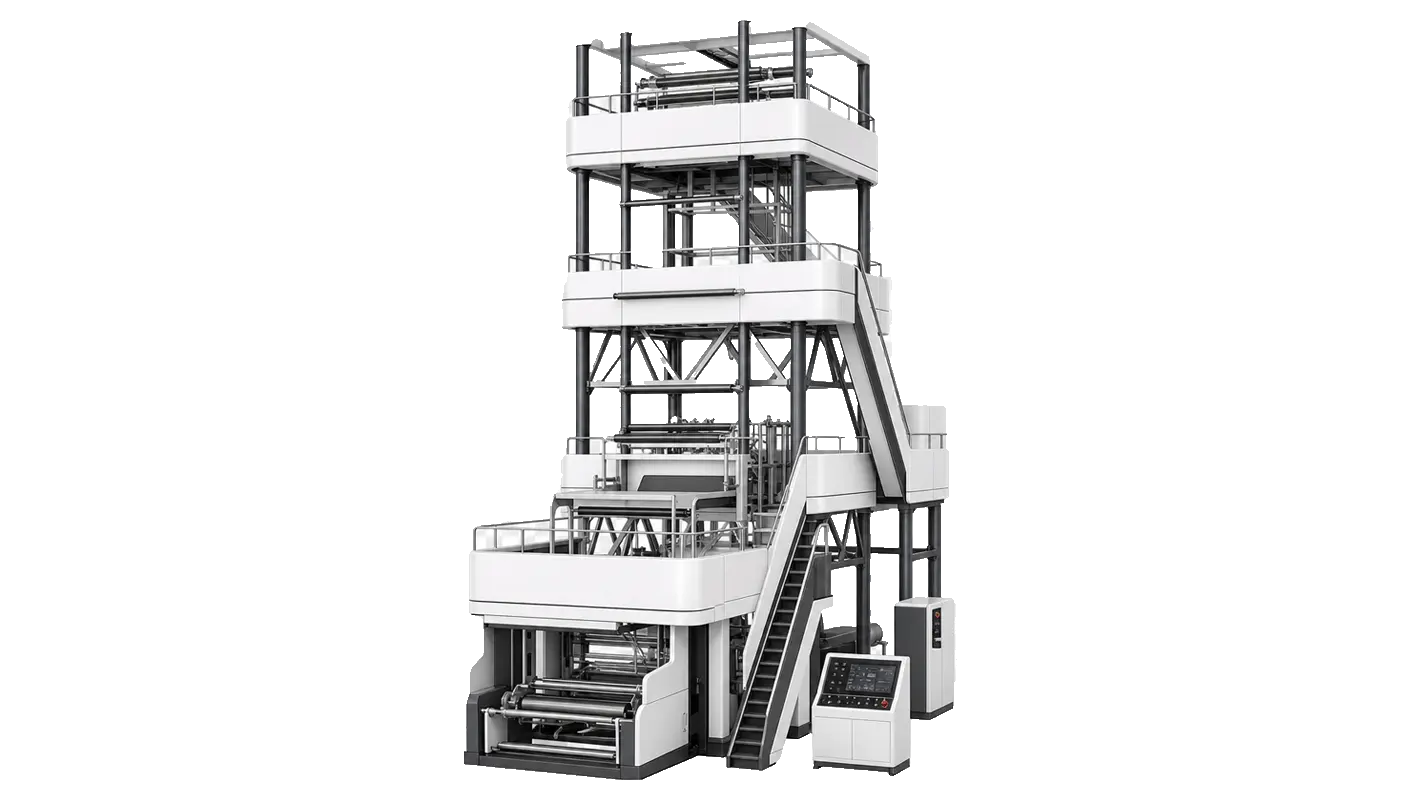
LayerQuestar 5-layer co-extrusion blown film machine — EVOH PA barrier film production line
5 Layers

5-Layer Co-Extrusion Blown Film Machine

Five independent extruders. Two proven barrier structures — PE/TIE/EVOH/TIE/PE for oxygen-sensitive food packaging, PE/TIE/PA/TIE/PE for puncture-resistant industrial film. Output range 100–600 kg/h depending on configuration.

5 Independent Extruders
100–600 kg/h Output Range
EVOH & PA Barrier Structures
72 hr Factory Run Test
123+ Patents Granted
Applications

What Does a 5-Layer Co-Extrusion Machine Produce?

A 5-layer co-extrusion blown film machine combines five independently controlled melt streams into a single multi-layer film structure. The result is film that performs functions no single-material film can achieve — barrier against oxygen and moisture, structural strength, and heat-sealability, all in one continuous web.

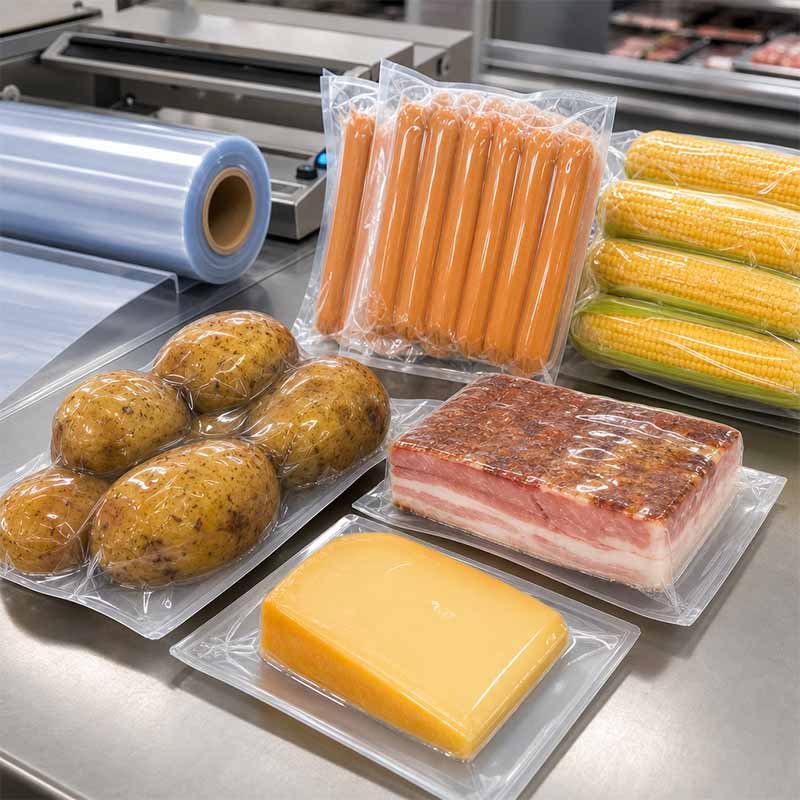
Flexible food packaging vacuum bags and retort pouches produced on a 5-layer EVOH blown film line
Primary Application

Food & Vacuum Packaging Film

The PE/TIE/EVOH/TIE/PE structure provides oxygen barrier performance required for vacuum bags, retort pouches, frozen food packaging and modified atmosphere packaging (MAP). EVOH in the center layer blocks oxygen transmission while the outer PE layers provide heat-seal performance and moisture resistance.

  • Vacuum packaging bags
  • Retort / cook-in pouches
  • Frozen food packaging
  • Modified atmosphere packaging (MAP)
  • Dairy and fresh produce film
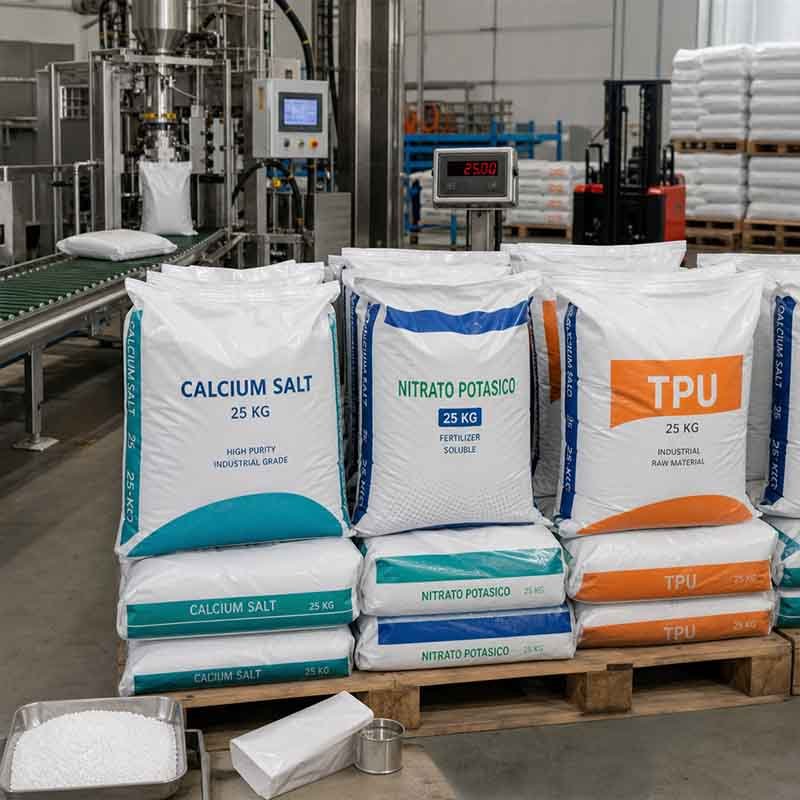
Heavy-duty industrial packaging sacks and chemical bags produced on a 5-layer PA blown film line
Primary Application

Heavy-Duty Industrial & Chemical Packaging

The PE/TIE/PA/TIE/PE structure uses a nylon (PA) core layer to deliver puncture resistance and mechanical strength beyond what PE alone can provide. Suitable for chemical products, agricultural inputs and industrial goods that require robust, reliable containment.

  • Chemical and fertilizer bags
  • Agricultural input packaging
  • Industrial heavy-duty sacks
  • Liner bags for bulk containers
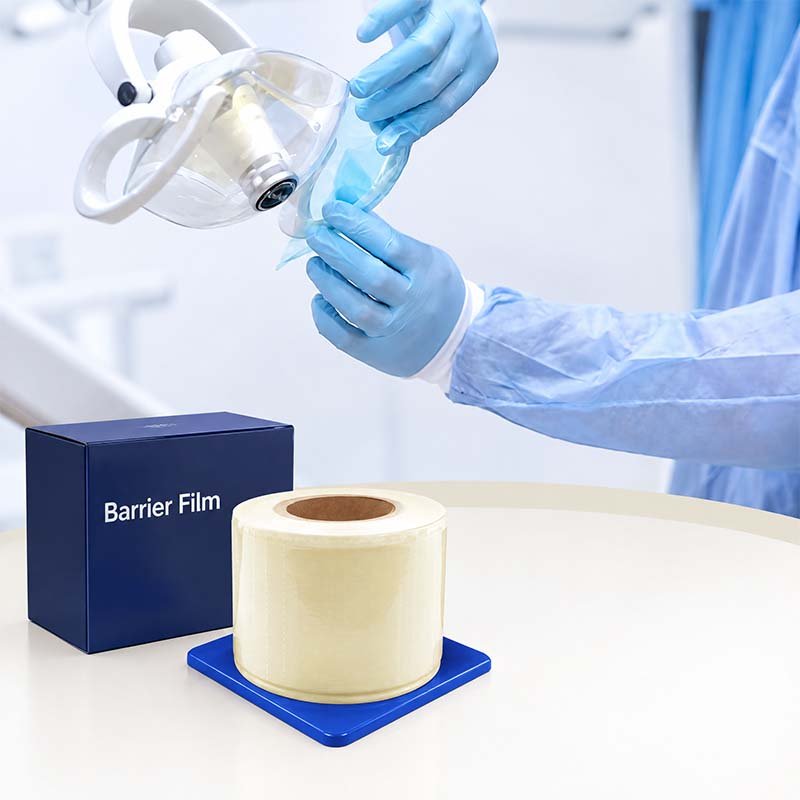
Medical packaging film and specialty barrier film produced on a 5-layer co-extrusion blown film machine
Specialty Application

Medical & Specialty Barrier Film

Multi-layer co-extrusion allows each layer to be assigned a distinct functional role — barrier, adhesion, structural, or surface performance. This makes 5-layer film suitable for medical device packaging, sterile barrier systems and specialty technical films where single-material structures are insufficient.

  • Medical device packaging film
  • Sterile barrier packaging
  • Greenhouse and agricultural functional film
  • High-clarity lamination base film

Five-layer co-extrusion is the established industry standard for flexible food packaging that requires both barrier performance and heat-seal capability. The symmetric TIE layer arrangement — one adhesive layer on each side of the barrier core — is what makes it possible to bond incompatible materials (EVOH or PA with PE) into a single, delamination-resistant film structure. LayerQuestar Machinery's 5-layer co-extrusion lines support both EVOH and PA core configurations, allowing converters to serve multiple market segments from a single machine platform.

Layer Architecture

Two Barrier Structures, One Machine Platform

LayerQuestar's 5-layer co-extrusion line supports two proven barrier architectures. Both use the same symmetric TIE layer logic — the choice of core material determines the barrier function the film delivers.

Structure A — Oxygen Barrier (EVOH)
Vacuum bags · Retort pouches · Food packaging · MAP
Layer 1 (A) PE / LLDPE Outer layer — moisture barrier, printable surface Layer 2 (B) TIE Adhesive layer — bonds PE to EVOH Layer 3 (C) EVOH Core barrier — blocks oxygen transmission Layer 4 (D) TIE Adhesive layer — bonds EVOH to PE Layer 5 (E) PE / LLDPE Inner layer — heat-seal surface Extruder A Extruder B Extruder C Extruder D Extruder E
Structure B — Puncture Resistance (PA / Nylon)
Heavy-duty sacks · Chemical bags · Industrial packaging
Layer 1 (A) PE / LLDPE Outer layer — moisture barrier, printable surface Layer 2 (B) TIE Adhesive layer — bonds PE to PA Layer 3 (C) PA (Nylon) Core layer — puncture resistance, mechanical strength Layer 4 (D) TIE Adhesive layer — bonds PA to PE Layer 5 (E) PE / LLDPE Inner layer — heat-seal surface Extruder A Extruder B Extruder C Extruder D Extruder E

Film Cross-Section — Typical Layer Thickness Ratio

Thickness ratios are reference values. Each extruder's screw speed is independently adjustable to modify layer proportions during production.

Structure A — EVOH
PE / LLDPE ~35%
TIE ~8%
EVOH ~10%
TIE ~8%
PE / LLDPE ~39%
PE / LLDPE — Structural & seal layers TIE — Adhesive layers EVOH — Oxygen barrier core
Structure B — PA (Nylon)
PE / LLDPE ~35%
TIE ~8%
PA ~10%
TIE ~8%
PE / LLDPE ~39%
PE / LLDPE — Structural & seal layers TIE — Adhesive layers PA — Puncture resistance core

Layer Function Reference

Layer Extruder Typical Material Primary Function Notes
Layer 1 A PE / LLDPE / mLLDPE Outer surface — moisture resistance, printability Can include slip or anti-block additives
Layer 2 B TIE (maleic anhydride grafted PE) Adhesive — bonds outer PE to barrier core Required when bonding incompatible materials
Layer 3 C EVOH or PA (Nylon) Core barrier — oxygen block (EVOH) or puncture resistance (PA) Smallest extruder — barrier layer is thin by design
Layer 4 D TIE (maleic anhydride grafted PE) Adhesive — bonds barrier core to inner PE Mirror of Layer 2 — symmetric structure
Layer 5 E PE / LLDPE / mLLDPE Inner surface — heat-seal layer Formulated for target seal temperature and strength

The TIE layer is the element most frequently misunderstood by buyers new to multi-layer film. EVOH and PA are chemically incompatible with standard PE — they will not bond without an adhesive resin between them. TIE resins (typically maleic anhydride grafted polyethylene) are specifically engineered to create a durable chemical bond between the PE outer layers and the barrier core. Without TIE layers, the film structure would delaminate under stress. In a 5-layer structure, two TIE layers are used — one on each side of the barrier core — creating a symmetric, stable construction. LayerQuestar Machinery's 5-layer die head is designed to maintain precise layer thickness ratios across all five channels simultaneously.

Technical Specifications

5-Layer Co-Extrusion Line — Model Range

LayerQuestar's 5-layer co-extrusion lines are available in LDPE/LLDPE and HDPE/LLDPE configurations. Select the model range that matches your target film width and output requirement.

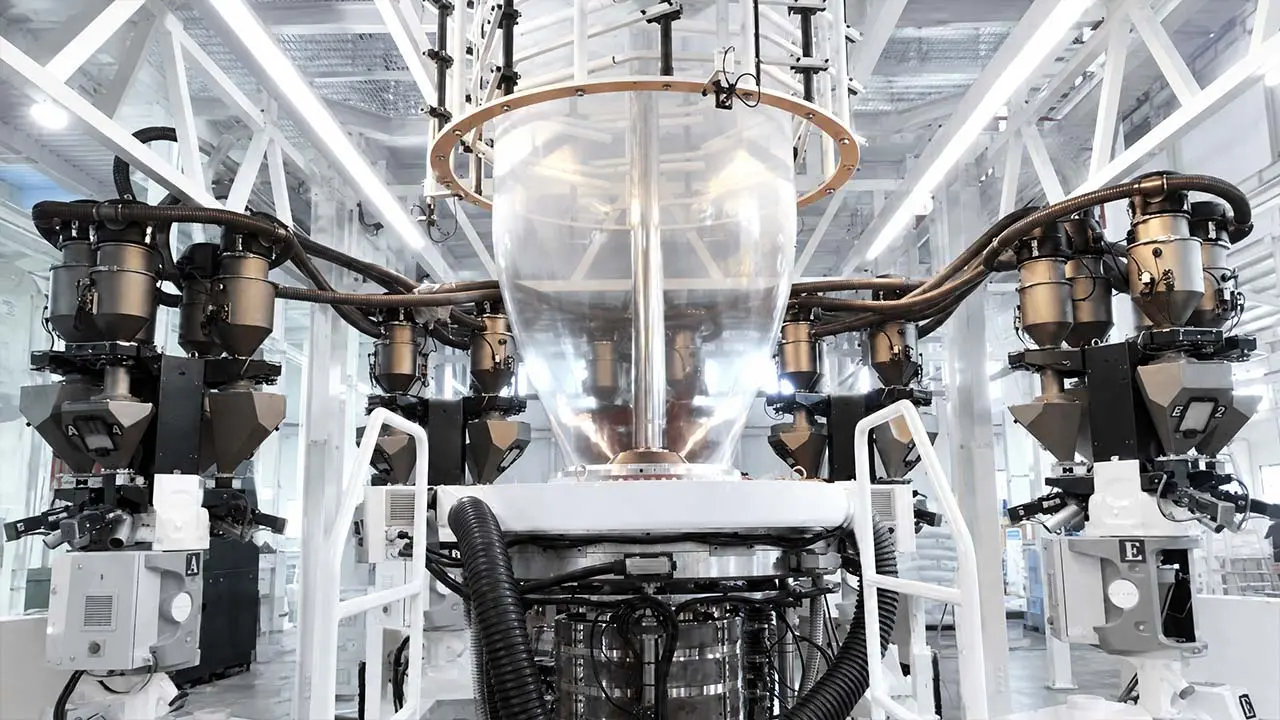
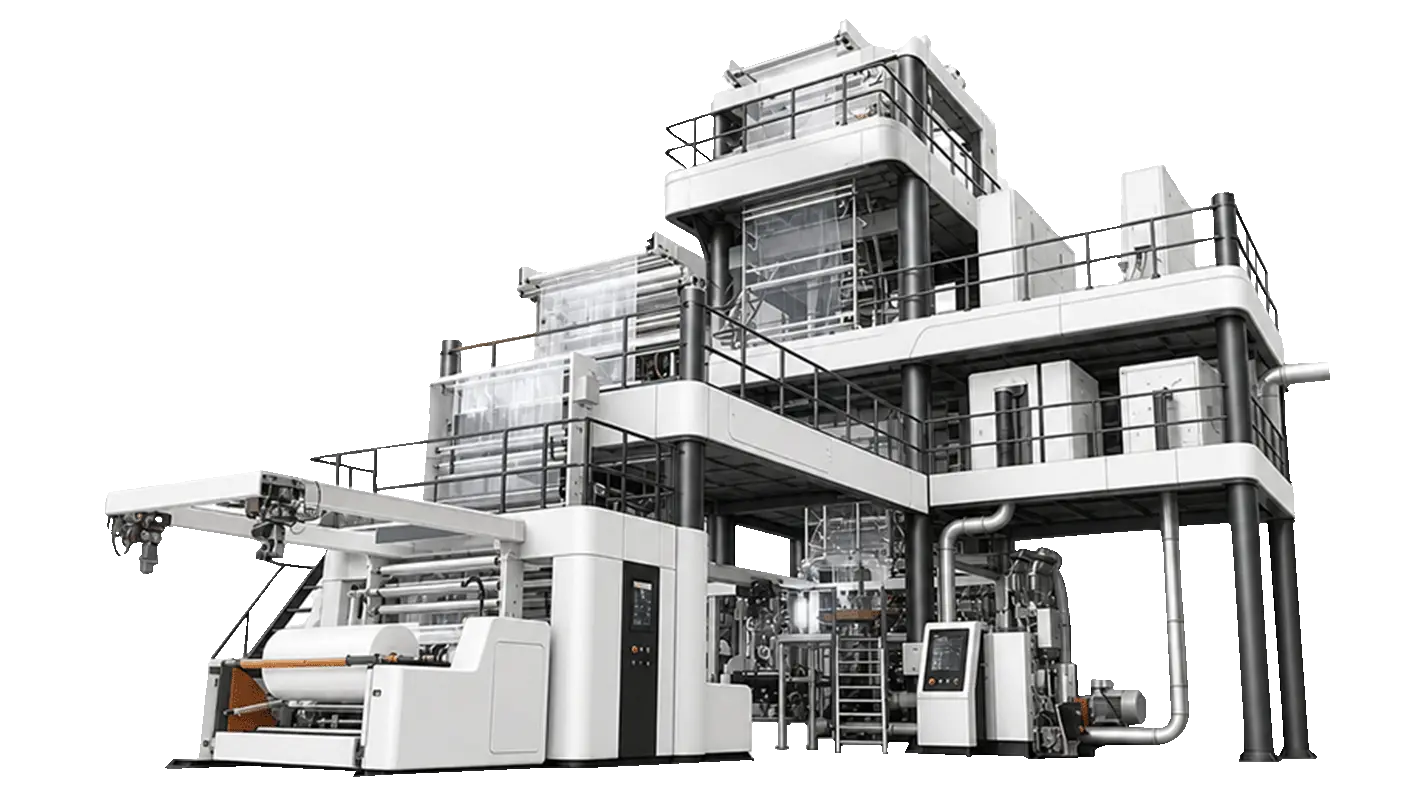
LayerQuestar 5-layer co-extrusion blown film machine — exterior view showing five extruders and die head
Model Material Output (kg/h) Motor Power (kW) Screw Diameter Max Layflat Width Cooling Fan (kW) Floor Space (m)
LQ-5L-1100 LDPE / LLDPE 120–160 15×2 / 18.5×1 / 15×2 Φ45/50/55/50/45 mm 100 mm 7.5 kW 9×6.5×8.0
LQ-5L-1300 LDPE / LLDPE 160–200 18.5×2 / 30×1 / 18.5×2 Φ50/55/60/55/50 mm 120 mm 7.5 kW 10×7×8.5
LQ-5L-1600 LDPE / LLDPE 200–250 22×2 / 37×1 / 22×2 Φ55/60/65/60/55 mm 150 mm 11 kW 11×7.5×9.0
LQ-5L-1800 LDPE / LLDPE 240–300 30×2 / 45×1 / 30×2 Φ60/65/70/65/60 mm 180 mm 11 kW 11×8×9.5
LQ-5L-2200 LDPE / LLDPE 280–350 37×2 / 55×1 / 37×2 Φ65/70/75/70/65 mm 220 mm 15 kW 12×8.5×10.0
LQ-5L-2500 LDPE / LLDPE 350–450 45×2 / 75×1 / 45×2 Φ70/80/85/80/70 mm 250 mm 15 kW 13×9×10.5
LQ-5L-3200 LDPE / LLDPE 450–600 55×2 / 90×1 / 55×2 Φ80/85/90/85/80 mm 650 mm 18.5 kW 14×10×11.5
Model Material Output (kg/h) Motor Power (kW) Screw Diameter Max Layflat Width Cooling Fan (kW) Floor Space (m)
LQ-5L-900 HDPE / LLDPE 100–120 15×2 / 18.5×1 / 11×2 Φ45/45/50/45/45 mm 80 mm 5.5 kW 8×6×7.5
LQ-5L-1100 HDPE / LLDPE 120–160 15×2 / 18.5×1 / 15×2 Φ45/50/55/50/45 mm 100 mm 7.5 kW 9×6.5×8.0
LQ-5L-1300 HDPE / LLDPE 160–200 18.5×2 / 30×1 / 18.5×2 Φ50/55/60/55/50 mm 120 mm 7.5 kW 10×7×8.5
LQ-5L-1600 HDPE / LLDPE 200–250 22×2 / 37×1 / 22×2 Φ55/60/65/60/55 mm 150 mm 11 kW 11×7.5×9.0
LQ-5L-1800 HDPE / LLDPE 240–300 30×2 / 45×1 / 30×2 Φ60/65/70/65/60 mm 180 mm 11 kW 11×8×9.5
LQ-5L-2200 HDPE / LLDPE 280–350 37×2 / 55×1 / 37×2 Φ65/70/75/70/65 mm 220 mm 15 kW 12×8.5×10.0
LQ-5L-2500 HDPE / LLDPE 280–350 37×2 / 55×1 / 37×2 Φ65/70/75/70/65 mm 250 mm 15 kW 13×9×10.5

Output figures are reference values under standard operating conditions and vary by film thickness, material formula and layflat width. Contact LayerQuestar for a configuration-specific proposal tailored to your product requirements.

Facility & Installation Reference

Power Supply

380V / 50Hz standard. 440V / 60Hz available on request. Confirm local supply before ordering.

Ceiling Height

Minimum 8.0m for mid-range models. Larger configurations (LQ-5L-2500 and above) require 10.5m or higher. Refer to model-specific floor space data above.

Raw Material Storage

Five separate material hoppers require dedicated storage areas for PE, TIE and EVOH or PA resins. EVOH and PA must be stored in dry conditions and pre-dried before processing.

Compressed Air

Required for bubble inflation and IBC (internal bubble cooling) system where fitted. Confirm air supply capacity with LayerQuestar during configuration.

Buyer Fit

Is a 5-Layer Line the Right Investment for You?

A 5-layer co-extrusion line is a significant step up in complexity and capital investment from a 3-layer machine. This section helps you determine whether the application genuinely requires 5-layer capability.

Good Fit

  • Your customers require food-grade packaging with measurable oxygen barrier performance
  • You are producing vacuum bags, retort pouches, MAP film or dairy packaging
  • Your application requires puncture resistance beyond what PE alone can provide
  • You are supplying chemical, agricultural or industrial goods in heavy-duty flexible packaging
  • You need to differentiate all five layers independently — different materials, different formulas
  • You are an existing converter upgrading from 3-layer to meet new customer or regulatory requirements

Consider Alternatives If...

  • Your product is shopping bags, courier bags or garbage bags — a 3-layer ABA or ABC machine is sufficient and more cost-effective
  • You do not need an EVOH or PA barrier layer — the additional extruders and die head complexity are not justified
  • Your budget is constrained and your product range does not require barrier performance — start with 3-layer and upgrade later
  • You need 7-layer asymmetric barrier structures or ultra-high barrier performance — consider the 7-layer EVOH barrier line

Layer Configuration Decision Guide

Your Requirement Recommended Configuration
Shopping bags, T-shirt bags, garbage bags Mono-Layer Machine →
Courier bags, lamination film, PCR isolation 3-Layer ABA/ABC Machine →
Food packaging with oxygen barrier (EVOH), heavy-duty industrial film (PA) 5-Layer Co-Extrusion Line — this page
Ultra-high barrier, asymmetric structures, extended shelf-life packaging 7-Layer EVOH Barrier Line →
PLA/PBAT compostable film Biodegradable Film Machine →
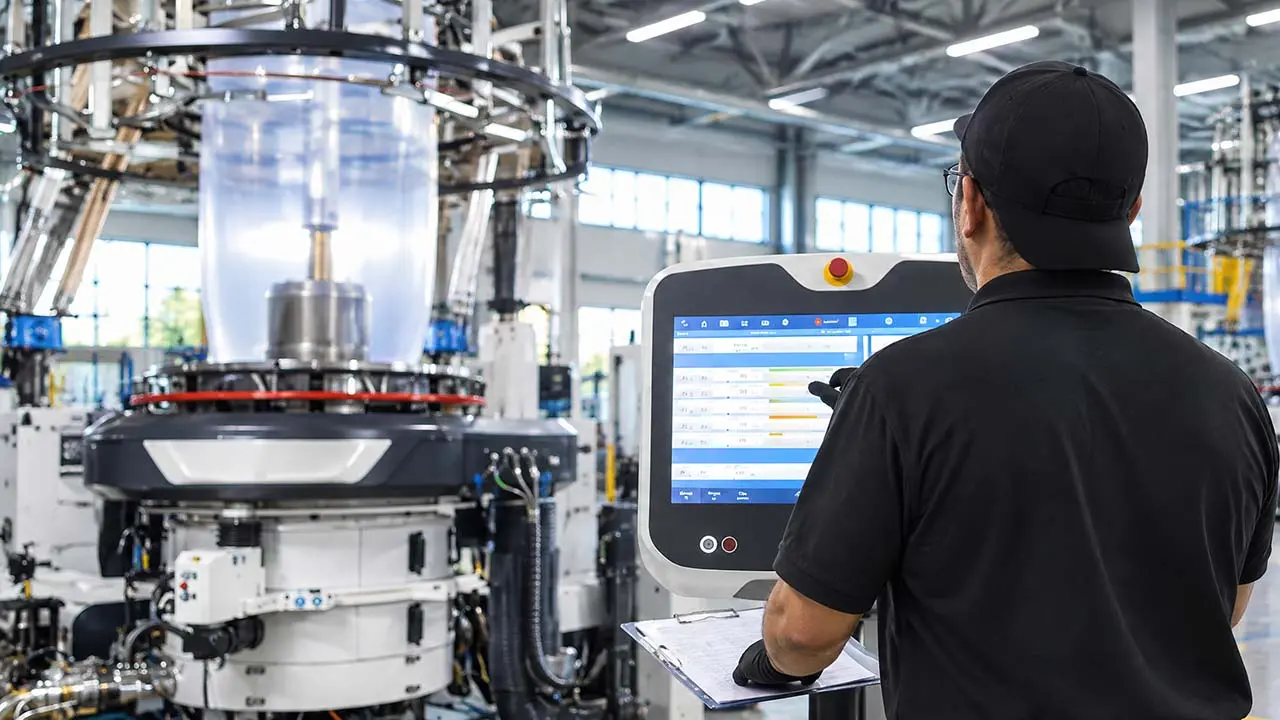
Operator running LayerQuestar 5-layer co-extrusion blown film line — monitoring five extruder control panels
Operation

Running a 5-Layer Co-Extrusion Line

A 5-layer line requires more operator attention than a 3-layer machine — five independent material streams, each with its own temperature profile, feed rate and screw speed. Here is what to plan for.

Operator Requirements

A 5-layer co-extrusion line typically requires 2–3 operators per shift under normal production conditions — one lead operator managing the five extruder control panels and die head, one winding/roll-change operator, and optionally one material handling assistant for the five separate resin hoppers. Prior experience with multi-layer extrusion is recommended for the lead operator role.

EVOH & PA Material Handling

EVOH and PA resins are moisture-sensitive. Both materials must be pre-dried before processing — EVOH typically at 80°C for 4–6 hours, PA at 80–85°C for 8–12 hours, depending on the specific grade and ambient humidity conditions. Failure to pre-dry will result in bubble instability, surface defects and reduced barrier performance. Dedicated drying hoppers for the C extruder are strongly recommended.

Layer Thickness Ratio Adjustment

Each extruder's screw speed can be adjusted independently to change the thickness ratio of individual layers without stopping production. The EVOH or PA core layer is typically set to 5–15% of total film thickness — enough to deliver barrier performance while minimising the cost of the most expensive resin in the structure. Operators can fine-tune ratios in response to material cost changes or customer specification adjustments.

Changeover & Purging

Switching between EVOH and PA core structures requires a full purge of the C extruder and die head C channel. EVOH is particularly sensitive to thermal degradation if left in the barrel at processing temperature without material flow. Purging protocols and maximum idle time limits should be established before production begins. LayerQuestar provides recommended purging procedures as part of the machine commissioning documentation.

Downstream Compatibility

5-layer barrier film rolls are compatible with downstream slitting, printing and bag making equipment. For food packaging applications, the film typically proceeds to a flexographic printer for surface printing, then to a bag making machine for pouch or bag conversion. Confirm downstream equipment specifications — particularly seal bar temperature settings — are calibrated for the specific film structure being produced.

Build Standard

How LayerQuestar Builds the 5-Layer Line

Every component specification in a LayerQuestar 5-layer co-extrusion line is selected for long-term reliability under continuous industrial operation. These are the hardware standards applied to every machine we build.

LayerQuestar 5-layer co-extrusion blown film machine factory acceptance test — 72-hour continuous run

72-Hour Factory Acceptance Test (FAT)

Every LayerQuestar 5-layer co-extrusion line runs a continuous 72-hour production test at our Zhejiang factory before shipment. During the FAT, all five extruders run simultaneously under load. Output consistency, temperature stability across all five zones, film thickness tolerance (±8% target), layer ratio accuracy, winding quality and all mechanical and electrical systems are verified and documented.

Buyers and their representatives are welcome to witness the FAT in person before final payment and dispatch. Test reports are provided with every machine.

National High-Tech Enterprise Provincial Innovative SME 123+ Patents Granted
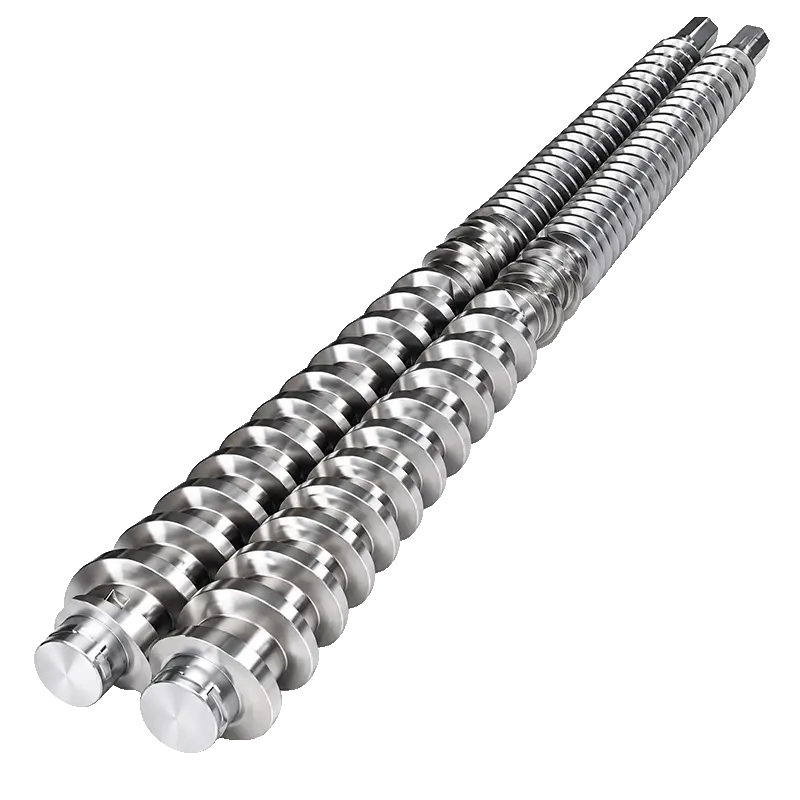
WC bi-metallic screw close-up — LayerQuestar 5-layer co-extrusion blown film machine

WC Bi-Metallic Screw

Base material: 38CrMoAlA nitrided steel. 1.5–3mm tungsten carbide alloy overlay on screw flight. HRC 59–65 surface hardness. Applied across all five extruders. Designed for long-term abrasion resistance when running filled compounds and recycled content blends.

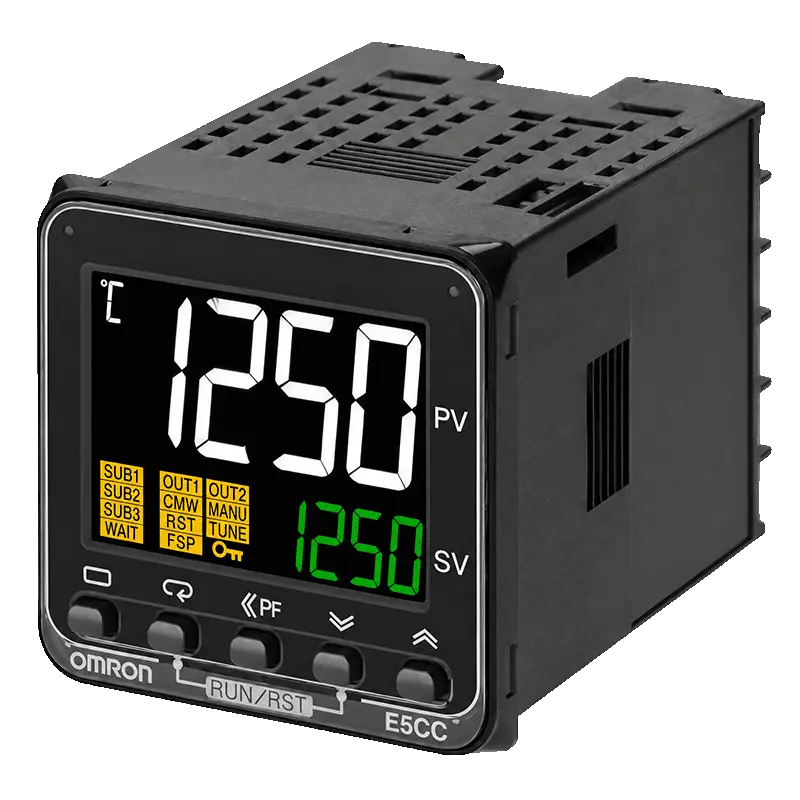
OMRON PID temperature controller close-up — LayerQuestar 5-layer co-extrusion blown film machine

OMRON PID Temperature Control

OMRON PID controllers fitted to all five extruder barrel zones and die head channels. Temperature deviation ±1°C under stable operating conditions. Critical for EVOH processing — EVOH has a narrow processing window and requires precise, consistent temperature control to maintain barrier integrity and avoid thermal degradation.

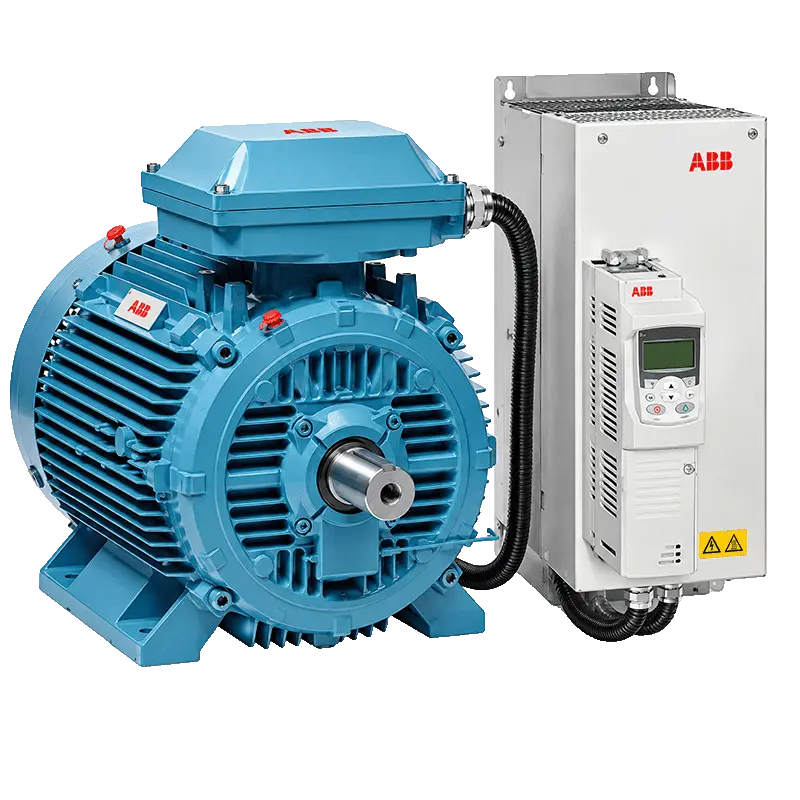
ABB main drive motor close-up — LayerQuestar 5-layer co-extrusion blown film machine

ABB Main Drive Motors

ABB motors are the preferred specification for all five extruder drives. Innomotics and other internationally recognised brands are available on request. Five independent variable-frequency drives allow each extruder's screw speed — and therefore each layer's output rate — to be adjusted independently during production.

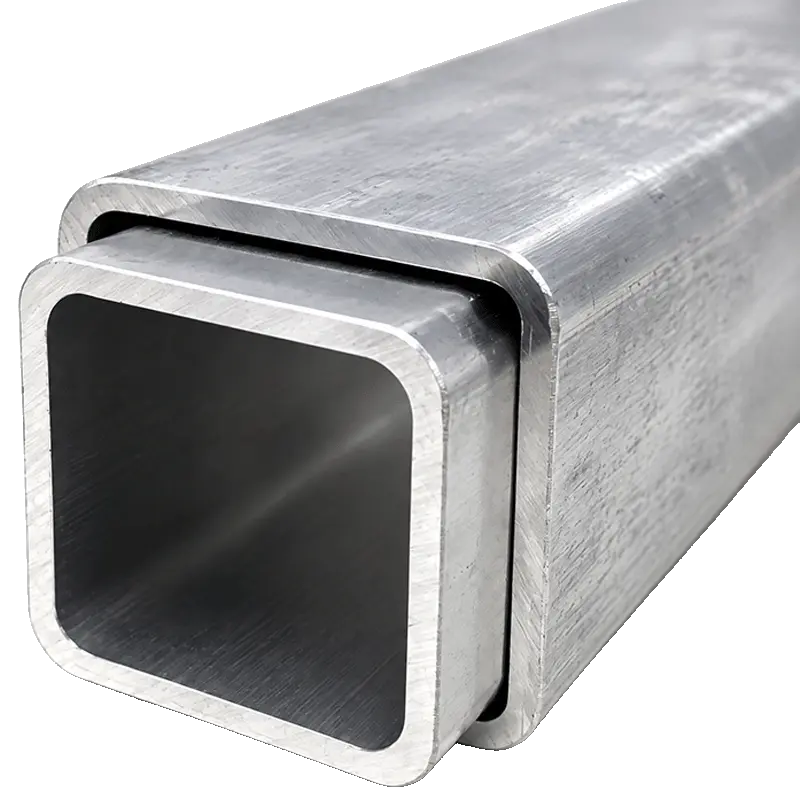
140mm heavy-wall square tube machine frame close-up — LayerQuestar 5-layer co-extrusion blown film machine

140mm Heavy-Wall Square Tube Frame

The machine frame is constructed from 140mm heavy-wall square steel tube throughout. A 5-layer line carries the combined weight and vibration load of five extruder assemblies — frame rigidity directly affects long-term alignment stability of the die head and winding system. This specification is applied consistently across all LayerQuestar co-extrusion line sizes.

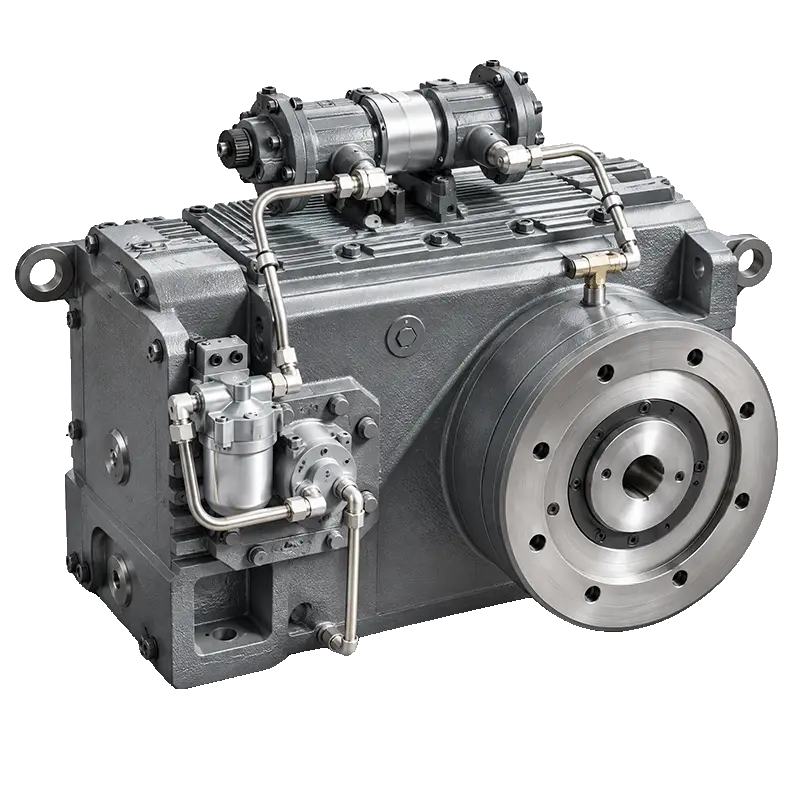
External oil-cooled circulation gearbox close-up — LayerQuestar 5-layer co-extrusion blown film machine

External Oil-Cooled Circulation Gearbox

Each of the five extruders is fitted with an external oil-cooled circulation gearbox, designed for 8–10 years of continuous service life under normal operating conditions. External oil cooling maintains consistent gearbox temperature during extended production runs, reducing thermal wear on gear surfaces and extending oil change intervals.

After-Sales

Support After Your Line Ships

A 5-layer co-extrusion line is a long-term production asset. LayerQuestar Machinery provides structured after-sales support to protect that investment from day one.

Warranty

12-month warranty on mechanical and electrical components from the date of commissioning. Warranty covers manufacturing defects and component failures under normal operating conditions. Consumable wear parts are excluded from warranty coverage.

Wear Parts Supply

Screw and barrel sets, die head components, heater bands, temperature sensors and other scheduled wear parts are held in stock at our Zhejiang facility. Parts are available for order independently of any service contract. Critical wear parts for 5-layer lines are stocked with priority given the higher component count versus single-extruder machines.

Remote Technical Support

Video call support is available for commissioning assistance, process troubleshooting and operator training. Our technical team can review live machine data, control panel readings and film samples remotely to diagnose issues without requiring an on-site visit. On-site commissioning and installation support is available — contact LayerQuestar for terms applicable to your location.

Documentation Package

Every machine ships with a complete English-language documentation package: operation manual, electrical schematics, spare parts list with part numbers, recommended maintenance schedule, and FAT test report. The control cabinet is fully English-labeled. Documentation in additional languages is available on request.

FAQ

5-Layer Co-Extrusion — Frequently Asked Questions

Questions buyers and engineers ask most often about 5-layer co-extrusion blown film machines and barrier film production.

What is the core difference between a 5-layer machine and a 3-layer machine?

A 3-layer machine produces film where all three layers are made from compatible materials — typically PE-family resins that bond to each other without adhesives. A 5-layer machine introduces a barrier core material (EVOH or PA) that is chemically incompatible with PE. Two additional TIE (adhesive) layers are required — one on each side of the barrier core — to bond the structure together. The result is a film that can block oxygen transmission or resist puncture at a level that PE alone cannot achieve. The trade-off is higher material cost, greater process complexity, and the need for five independent extruders and a 5-channel die head.

What is the difference between EVOH and PA as a barrier core? Which should I choose?

EVOH (ethylene vinyl alcohol) is selected primarily for its oxygen barrier performance. It is the standard choice for food packaging applications where extending shelf life by blocking oxygen transmission is the primary requirement — vacuum bags, retort pouches, MAP film and dairy packaging are typical examples.

PA (polyamide / nylon) is selected primarily for mechanical performance — puncture resistance, abrasion resistance and tensile strength. It is the standard choice for heavy-duty industrial packaging where the film must withstand rough handling, sharp edges or heavy loads. Chemical bags, fertilizer packaging and industrial liner bags are typical examples.

The two materials are not interchangeable — they serve different performance requirements. LayerQuestar's 5-layer line supports both configurations. If your application requires both oxygen barrier and puncture resistance simultaneously, contact us to discuss 7-layer structures that can combine both functions.

What is a TIE layer and why is it necessary?

A TIE layer is a thin adhesive resin layer — typically maleic anhydride grafted polyethylene — that creates a chemical bond between two otherwise incompatible materials. PE and EVOH will not bond to each other directly; without a TIE layer between them, the film structure would delaminate under mechanical stress or during heat sealing.

In a 5-layer PE/TIE/EVOH/TIE/PE structure, two TIE layers are used — one between the outer PE and the EVOH core, and one between the EVOH core and the inner PE. This symmetric arrangement ensures the barrier core is fully bonded on both sides, creating a stable, delamination-resistant film. The TIE layer is typically very thin (5–10% of total film thickness) but is essential to the structural integrity of the film.

Can a 5-layer machine run standard PE film without EVOH or PA?

Technically yes — a 5-layer machine can run PE-only structures by feeding compatible PE-family resins into all five extruders. However, this is not an economically rational use of the machine. A 5-layer co-extrusion line carries significantly higher capital cost, operating complexity and maintenance requirements than a 3-layer machine. Running it on standard PE film means paying for capability you are not using.

If your current and foreseeable product range does not require EVOH or PA barrier layers, a 3-layer ABA or ABC machine is the more appropriate investment. Contact LayerQuestar and we will recommend the configuration that matches your actual production requirements.

Does EVOH have special temperature requirements during processing?

Yes. EVOH has a narrower processing window than PE and is sensitive to both under-heating and over-heating. Processing temperatures typically range from 190°C to 230°C depending on the specific EVOH grade and ethylene content — lower ethylene content grades generally require higher processing temperatures. EVOH is also sensitive to moisture: it must be pre-dried before processing (typically at 80°C for 4–6 hours) and should be protected from ambient humidity during storage and feeding.

Critically, EVOH degrades if left in the barrel at processing temperature without material flow. If production is interrupted, the EVOH extruder must be purged promptly. LayerQuestar's OMRON PID temperature control system — with ±1°C deviation under stable conditions — is specified in part to meet the precise temperature management requirements of EVOH processing.

Why is the centre extruder (Extruder C) smaller than the outer extruders?

The centre extruder (C) feeds the EVOH or PA barrier core layer, which is intentionally kept thin — typically 5–15% of total film thickness. EVOH and PA are significantly more expensive than PE, so minimising their proportion while maintaining barrier performance is a key part of the film cost structure. A smaller screw diameter on Extruder C is correctly matched to this lower output requirement.

The outer PE layers (Extruders A and E) carry the majority of the film's total thickness and require higher output capacity — hence the larger screw diameters. This asymmetric extruder sizing is standard practice in 5-layer barrier film line design and is reflected in LayerQuestar's model specifications.

Can I adjust the thickness ratio of each layer during production?

Yes. Each extruder's screw speed is independently controlled via its variable-frequency drive. Adjusting the screw speed of any individual extruder changes that layer's output rate and therefore its proportion of the total film thickness. This can be done while the line is running without stopping production.

In practice, operators adjust layer ratios in response to changes in raw material costs, customer specification requirements, or film performance targets. The EVOH or PA core layer ratio is typically the most actively managed — increasing it improves barrier performance but raises material cost, while reducing it lowers cost but may reduce barrier performance below specification.

How many operators does a 5-layer co-extrusion line require?

Under normal production conditions, a 5-layer co-extrusion line typically requires 2–3 operators per shift. A lead operator manages the five extruder control panels, die head and process parameters. A second operator handles winding, roll changes and film quality monitoring. A third operator — optional depending on line size and production pace — manages material feeding across the five hoppers and assists with roll handling.

Prior experience with multi-layer extrusion is recommended for the lead operator role, particularly for EVOH processing where temperature management and purging protocols are critical. LayerQuestar provides operator training as part of the commissioning process and remote training support is available after installation.

Get Started

Ready to Specify Your
5-Layer Co-Extrusion Line?

Tell us your target film structure, output requirement and product application. LayerQuestar Machinery will recommend the right model and configuration for your production goals.

Response within 1 business day · info@layerquestar.com