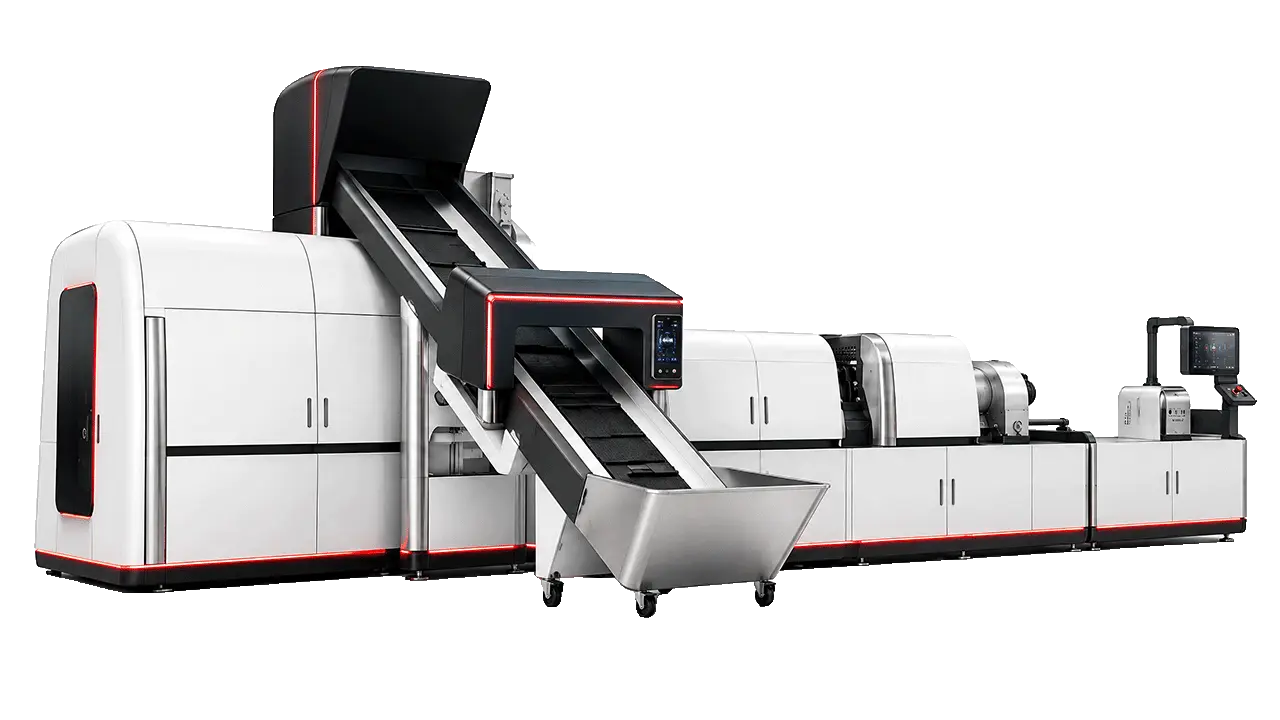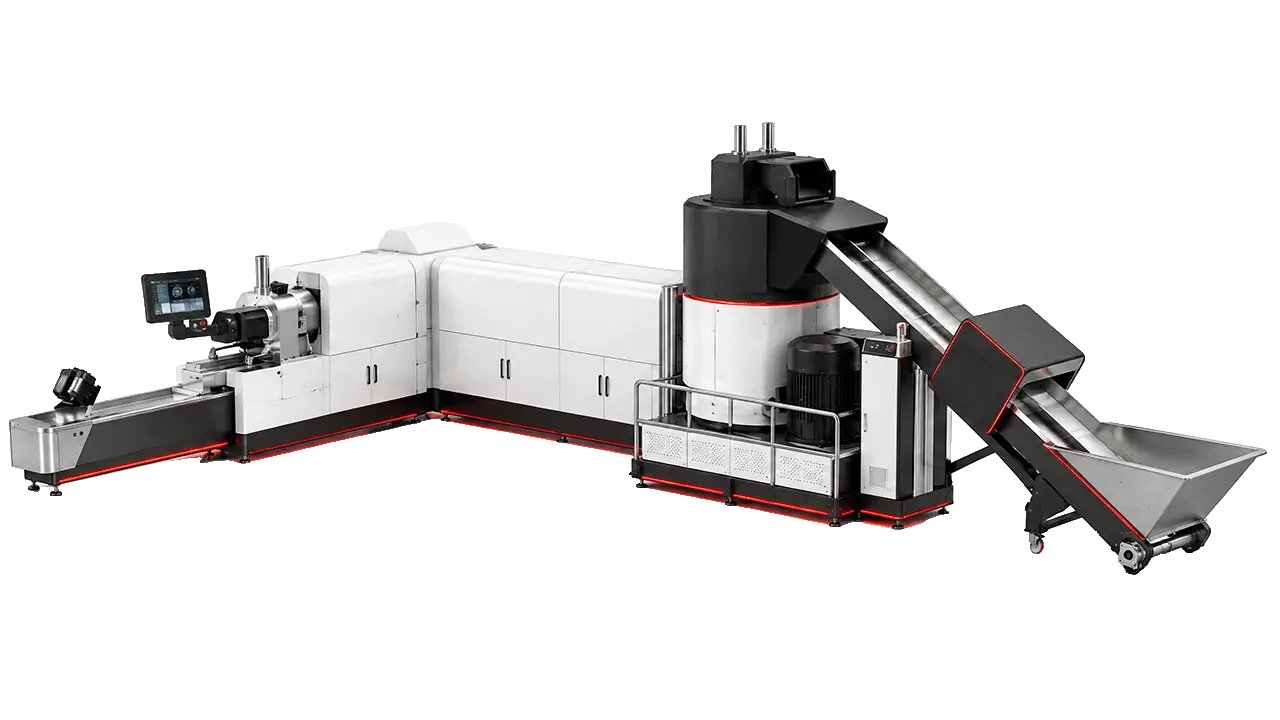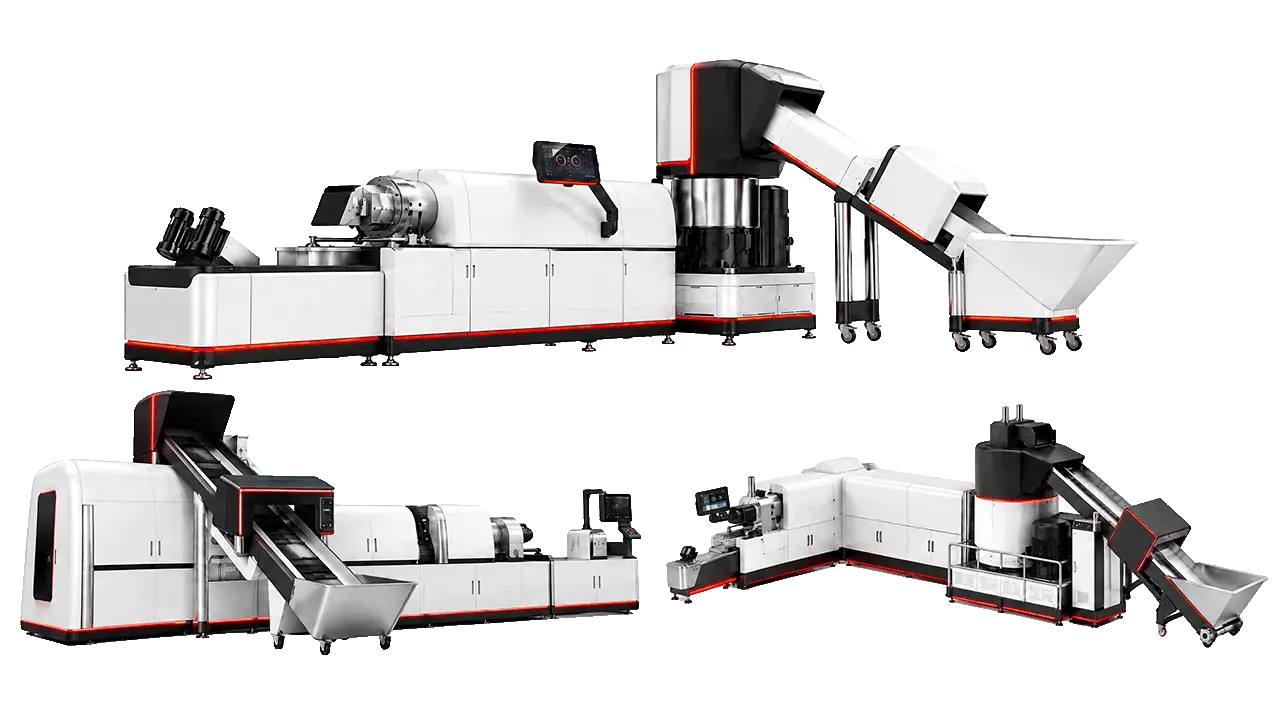
Convert blown film edge trim, roll waste and lightly printed scrap into reusable PE pellets — and feed them directly back into your production line. Dry-process systems for in-house industrial waste, 50 to 500 kg/h.
The right solution depends on one number: your daily waste volume. A standalone pelletizing line is not always the most efficient answer.
A side waste recycling unit with force feeder mounts directly alongside your blown film machine. Edge trim is ground and fed back into the extruder in real time — no separate pelletizing step, no storage, no handling.
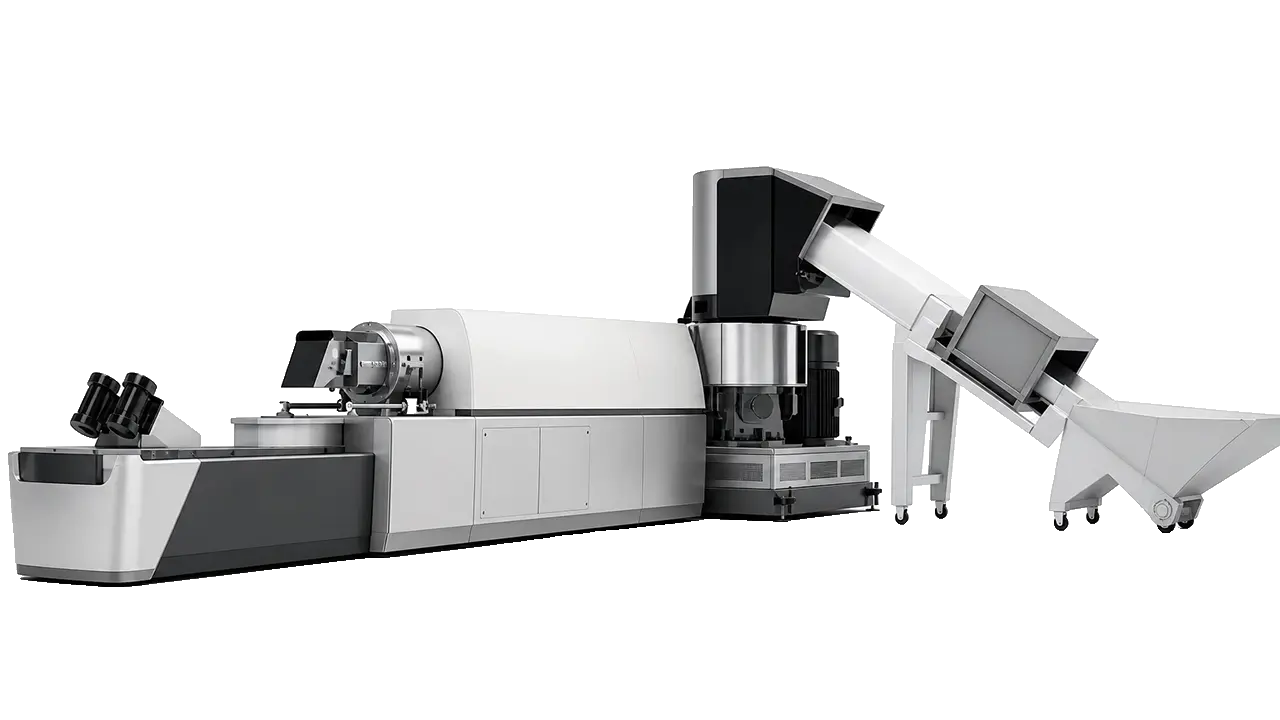
A dedicated recycling line handles waste from multiple blown film machines, processes lightly printed scrap, and produces uniform pellets for controlled blending back into production. This page covers this option in full.
Not sure which applies to you? Share your daily waste volume and number of blown film machines — LayerQuestar Machinery will recommend the right approach.
This line is designed for dry-process recycling of in-house industrial PE film waste. It is not designed for heavily contaminated post-consumer film or material requiring pre-washing — those applications require a different process.
Clean, unprinted edge trim from blown film lines and rejected rolls. Consistent material, low contamination. Single-stage system is sufficient.
Film produced during machine start-up, grade changeover and thickness adjustment. May contain minor thickness variation but is otherwise clean material.
Printed film waste with up to approximately 30% ink coverage. Ink volatiles require adequate degassing zones to prevent bubble formation in pellets.
Post-consumer film with soil, organic matter or heavy print requires pre-washing before pelletizing. This dry-process line is not designed for that application.
Getting these two decisions right determines whether your recycling line produces consistent, usable pellets — or runs into feeding problems and pellet quality issues from day one.
Loose PE film has very low bulk density — it compresses, bridges and starves a standard screw feeder. The feeding system must solve this before extrusion begins.
A rotating cutter drum shreds and frictionally heats loose film, compacting it into a dense, semi-molten mass that feeds directly and consistently into the extruder throat. Eliminates bridging and air pockets.
A belt conveyor transports pre-shredded or denser material into a force feeder that pushes it into the extruder. Suitable when material already has sufficient bulk density to feed reliably.
The primary factor is contamination level — specifically ink coverage and moisture content. When in doubt, a two-stage system produces better pellet quality at higher equipment cost.
| Criteria | Single-Stage | Two-Stage |
|---|---|---|
| Typical waste type | Clean or lightly printed in-house film | Moderately printed film (30–100% coverage) |
| Print coverage | Up to ~30% | 30–100% |
| Degassing zones | 2 zones | 3 zones |
| Filtration passes | Single pass | Double pass |
| Pellet purity | Standard | Enhanced |
| Typical applications | Factory edge trim, start-up purge, roll waste | Printed bag waste, mixed scrap streams |
| Reference output range | 50–400 kg/h varies by configuration | 100–500 kg/h varies by configuration |
If your waste stream includes both clean trim and printed scrap, specify for the more demanding material. A two-stage system handles both; a single-stage system cannot be easily upgraded after installation.
Understanding each stage helps you evaluate whether a proposed configuration is correctly specified for your waste type — and what to ask a supplier before you buy.
Loose film is fed into a rotating cutter drum. Friction and cutting action shred and heat the film, compacting it into a dense, semi-molten mass. This solves the fundamental problem of low bulk density in thin PE film — without this stage, the extruder screw cannot feed consistently.
Critical for thin film under 0.10 mmThe compacted material enters the extruder and is melted under controlled temperature and shear. Dedicated degassing zones (2 for single-stage, 3 for two-stage) vent moisture and ink volatiles from the melt. Inadequate degassing is the most common cause of bubbles and black specks in recycled PE pellets.
Degassing zone count must match your ink coverage levelThe melt passes through a screen changer that removes solid contaminants — paper labels, dust, non-PE particles. A continuous (non-stop) screen changer allows screen replacement without halting production. Two-stage systems pass the melt through a second filtration stage for enhanced purity.
Continuous type recommended — stop-type causes pressure surgesA gear pump installed after the screen changer stabilises melt pressure before the die, reducing pellet size variation. Recommended for applications where pellet uniformity is critical for downstream blend-back quality.
Adds cost; most in-house recycling applications do not require itThe filtered melt is extruded through a die plate and cut by rotating blades at the die face. Water-ring cooling solidifies the pellets immediately. Output is uniform cylindrical or lenticular pellets, dried and ready for blending back into your blown film line. Strand pelletizing is available as an alternative for specific applications.
Output: uniform pellets, ready for direct blend-backThe following specifications represent the standard configuration range. Final specifications are determined by your waste type, daily volume and output requirements.
| Parameter | Single-Stage System | Two-Stage System |
|---|---|---|
| Materials processed | LDPE, HDPE, LLDPE, mLLDPE, PCR PE blends | |
| Output range | 50–400 kg/h | 100–500 kg/h |
| Feeding system | Cutter-compactor (standard); belt conveyor + force feeder (option) | |
| Degassing zones | 2 zones | 3 zones |
| Filtration | Continuous screen changer, single pass | Continuous screen changer, double pass |
| Pelletizing method | Water-ring (standard); strand pelletizing (option) | |
| Applicable film thickness | 0.01–0.20 mm | |
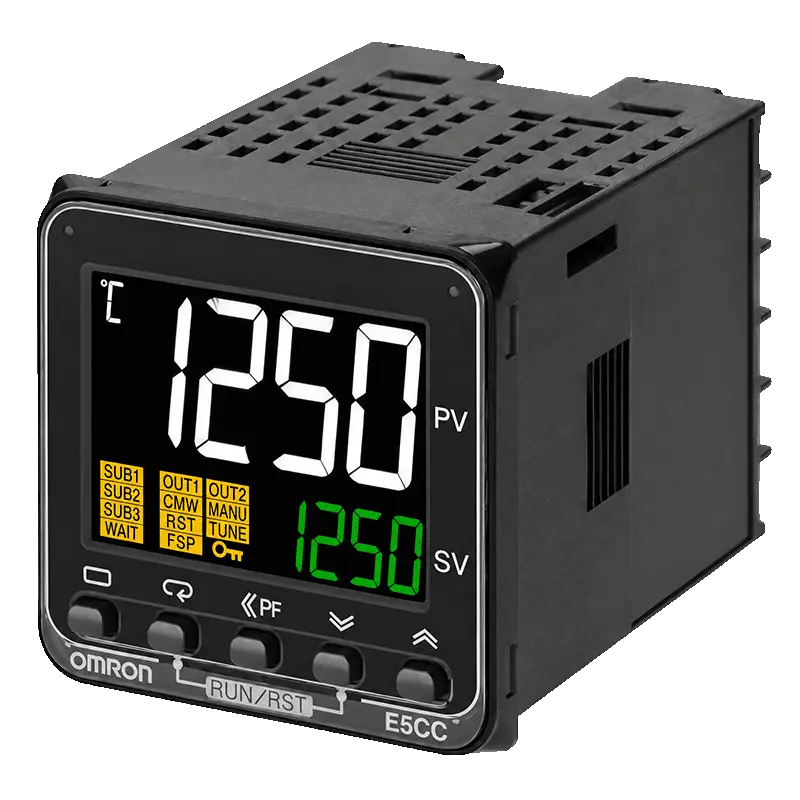
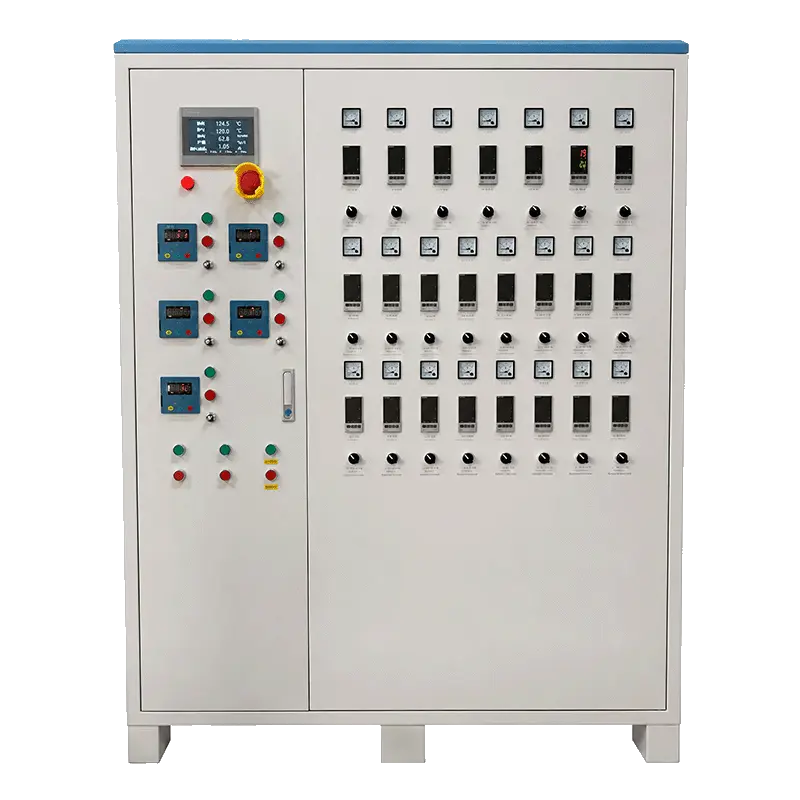
| Temperature control | OMRON PID; deviation ±1°C under stable conditions | |
| Control system | PLC with touch screen; English-labeled control cabinet | |
| Pellet shape | Cylindrical / lenticular (water-ring); cylindrical strand (strand option) | |
| Pre-shipment test | 72-hour continuous factory run test | |
All specifications subject to final application review. Output figures are reference ranges under standard operating conditions and vary by material formula, film thickness and contamination level. Contact LayerQuestar Machinery to confirm the right configuration for your specific waste stream.
LayerQuestar Machinery supplies PE film recycling lines designed for mid-scale flexible packaging factories — typically 1 to 5 blown film lines, with daily waste volumes of 100 to 2,000 kg. Internationally sourced components at a price point and lead time suited to factories in Southeast Asia, the Middle East, Africa and South America.
Every PE film recycling line runs a 72-hour continuous production test at LayerQuestar's factory before shipment. The test verifies output rate, pellet quality, temperature stability and control system function under sustained operating conditions. You or your representative are welcome to witness the test in person before final payment and dispatch.
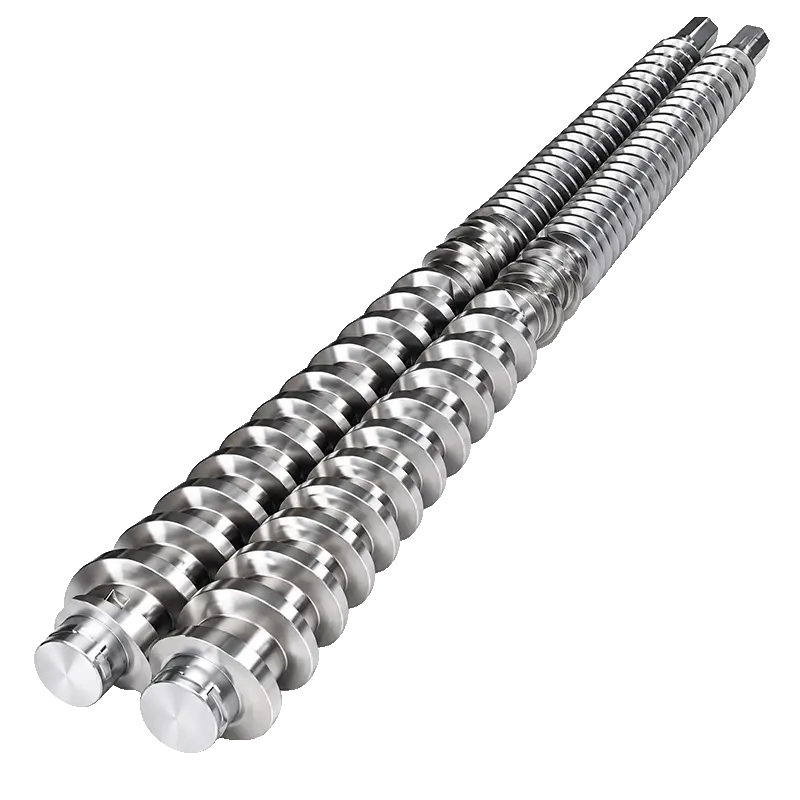
Base material: 38CrMoAlA nitrided steel. Surface: 1.5–3mm tungsten carbide alloy overlay, HRC 59–65. Designed for abrasive recycled material with contaminant particles.
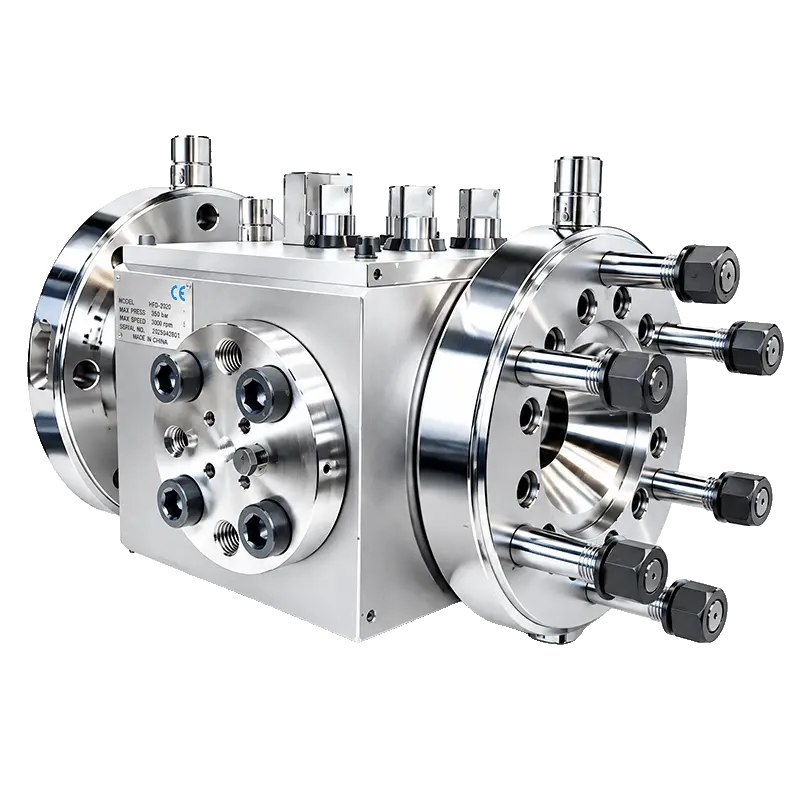
Non-stop screen replacement without halting production. Prevents pressure surges that cause pellet size variation. Critical for contaminated recycled material streams.
Zone-by-zone temperature control with ±1°C deviation under stable operating conditions. Consistent melt temperature is critical for uniform pellet quality in recycled material processing.
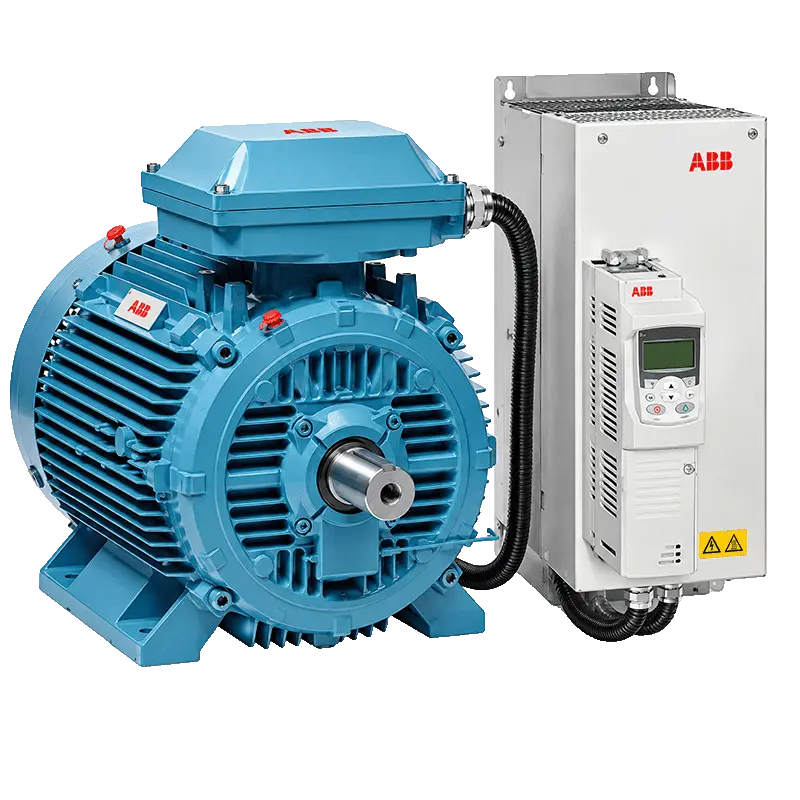
ABB motors preferred as standard. Innomotics and other international brands available depending on project requirements. Inverter-controlled for variable speed and energy efficiency.
All labels, indicators and documentation in English. 2–3 independent cooling fans. Designed for operation in factories where maintenance staff are not Chinese-speaking.
Answers to the questions factory owners and procurement managers ask most often before specifying a PE film recycling and pelletizing line.
This dry-process line is designed for in-house industrial PE film waste: LDPE, HDPE, LLDPE and mLLDPE blown film in the form of edge trim, roll waste, start-up purge and lightly printed scrap (up to approximately 30% ink coverage). It is not designed for heavily contaminated post-consumer film, agricultural mulch film with soil loading, or material requiring pre-washing. Those applications require a wet-process line with an upstream washing and drying stage.
Yes, with the correct degassing configuration. For film with up to approximately 30% ink coverage, a single-stage system with two degassing zones is typically sufficient. For film with 30–100% print coverage, a two-stage system with three degassing zones and double-pass filtration is required to achieve acceptable pellet quality. If you are unsure of your average ink coverage, specify for the higher contamination level — a two-stage system handles both clean and printed film, while a single-stage system cannot be easily upgraded after installation.
A cutter compactor is a feeding device that uses a rotating cutter drum to simultaneously shred and frictionally heat loose film, compacting it into a dense, semi-molten mass before it enters the extruder. Thin PE film has very low bulk density — loose edge trim and roll waste cannot feed consistently into a standard screw extruder. Without a cutter compactor, the screw feeds air instead of material, causing surging, inconsistent output and poor pellet quality. For most PE film recycling applications, a cutter compactor is not optional — it is a fundamental requirement of the feeding system.
Water-ring pelletizing cuts the melt at the die face and immediately cools the pellets in a water ring — producing lenticular or cylindrical pellets in a continuous, high-speed process. It is the standard choice for PE film recycling because it handles the low melt viscosity of LDPE and LLDPE well and produces a consistent pellet shape. Strand pelletizing extrudes the melt as strands, cools them in a water bath, then cuts them into pellets. It produces more uniform cylindrical pellets but requires stable melt pressure and is more sensitive to viscosity variation in recycled material. For most in-house PE film recycling applications, water-ring pelletizing is the more practical choice.
A single-stage system extrudes, degasses and pelletizes in one pass. It is suitable for clean or lightly contaminated in-house film waste with up to approximately 30% print coverage. A two-stage system passes the melt through a second extrusion and filtration stage, providing an additional degassing zone and a second filtration pass. This produces higher-purity pellets from more demanding waste streams — moderately to heavily printed film, or mixed scrap with variable contamination. Two-stage systems cost more and consume more energy, but produce pellets that are more consistently suitable for blend-back into production film.
Yes, with controlled blending. Recycled PE pellets from a correctly specified line are compatible with standard blown film extrusion conditions. They are typically blended with virgin resin at a ratio determined by the target application and film quality requirements. For non-food industrial film, garbage bags and heavy-duty sacks, higher recycled content ratios are commonly used. For applications with surface quality, print registration or optical clarity requirements, a lower blend ratio is standard. The blend ratio should be established through trial runs after the recycling line is commissioned — it is not a fixed number.
Start with your total blown film line throughput and your scrap rate. As a reference: a blown film line producing 200 kg/h running 20 hours per day generates 4,000 kg of film per day. At a 5% scrap rate, that is 200 kg of recyclable waste per day. If your recycling line runs 8 hours per day, you need a minimum output capacity of 25 kg/h — well within the range of a small single-stage system. For a factory with three blown film lines at similar throughput, the daily waste volume triples, and the recycling line capacity must be sized accordingly. Share your line count, throughput per line and estimated scrap rate with LayerQuestar Machinery and we will size the system for your specific situation.
Not with a continuous screen changer. A continuous (non-stop) screen changer allows the operator to replace the screen while the line continues running at full output. A stop-type screen changer requires a brief production halt and causes a pressure surge when restarted, which can affect pellet quality in the minutes immediately after changeover. For recycled PE film — which typically has higher contamination than virgin material and therefore requires more frequent screen changes — a continuous screen changer is strongly recommended. It is included as standard in LayerQuestar Machinery's PE film recycling line configuration.
Bubbles in pellets are almost always caused by insufficient degassing — moisture or ink volatiles that were not fully vented from the melt before pelletizing. The first step is to verify that all degassing zone vents are open and unobstructed, then check whether the throughput rate has been increased beyond the system's degassing capacity. Black specks typically indicate either thermally degraded material from overheating at a specific zone, or carbon contamination from ink pigments that were not fully filtered. Check the temperature profile for any zone running above specification, and verify the screen changer is not partially blocked and bypassing contaminated melt. If the problem persists after these checks, contact LayerQuestar Machinery's after-sales team with your temperature log and screen change frequency data.
Not reliably. A standard blown film extruder is designed for clean, consistent virgin or blended resin in pellet or powder form. It lacks the degassing zones required to handle moisture and ink volatiles in recycled film, the hardened screw and barrel needed to withstand abrasive contaminants, and the continuous screen changer required for contaminated melt filtration without production interruption. Attempting to process recycled film through a standard blown film extruder typically results in poor pellet quality, accelerated screw and barrel wear, and frequent production stoppages. A dedicated recycling line with the correct feeding, degassing and filtration configuration is the correct solution.
Share four things: your waste type (edge trim / printed scrap / mixed), estimated daily volume in kg, number of blown film lines, and your factory location. LayerQuestar Machinery will come back with a specific system recommendation — single or two-stage, feeding system, and reference capacity range.