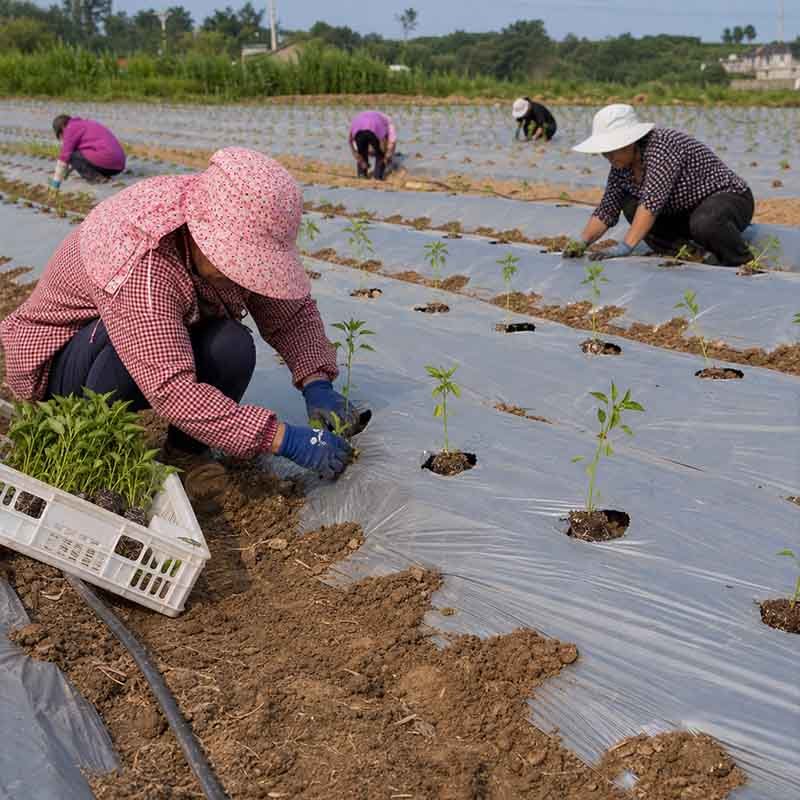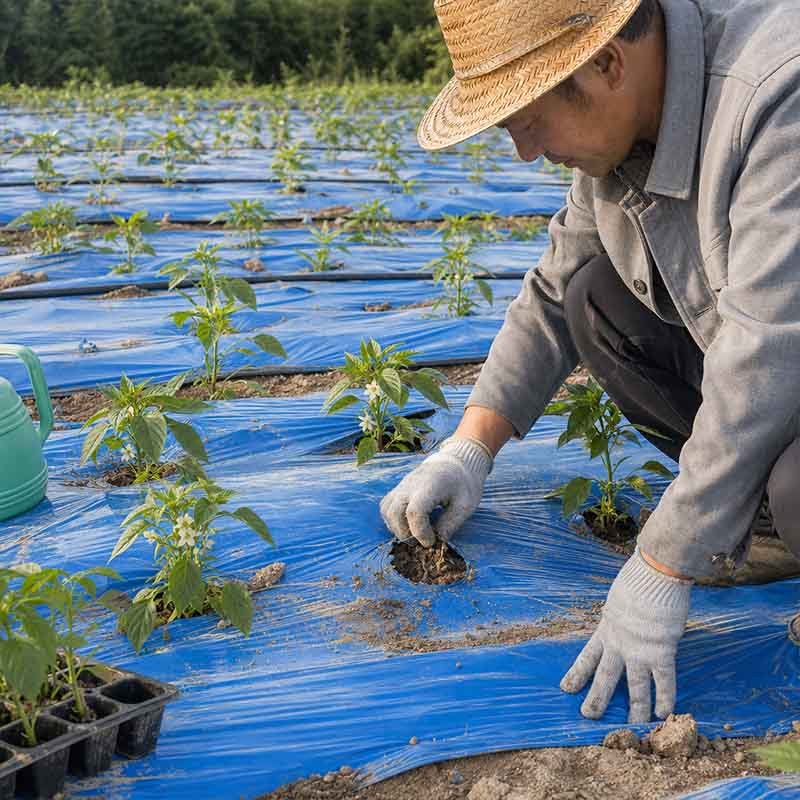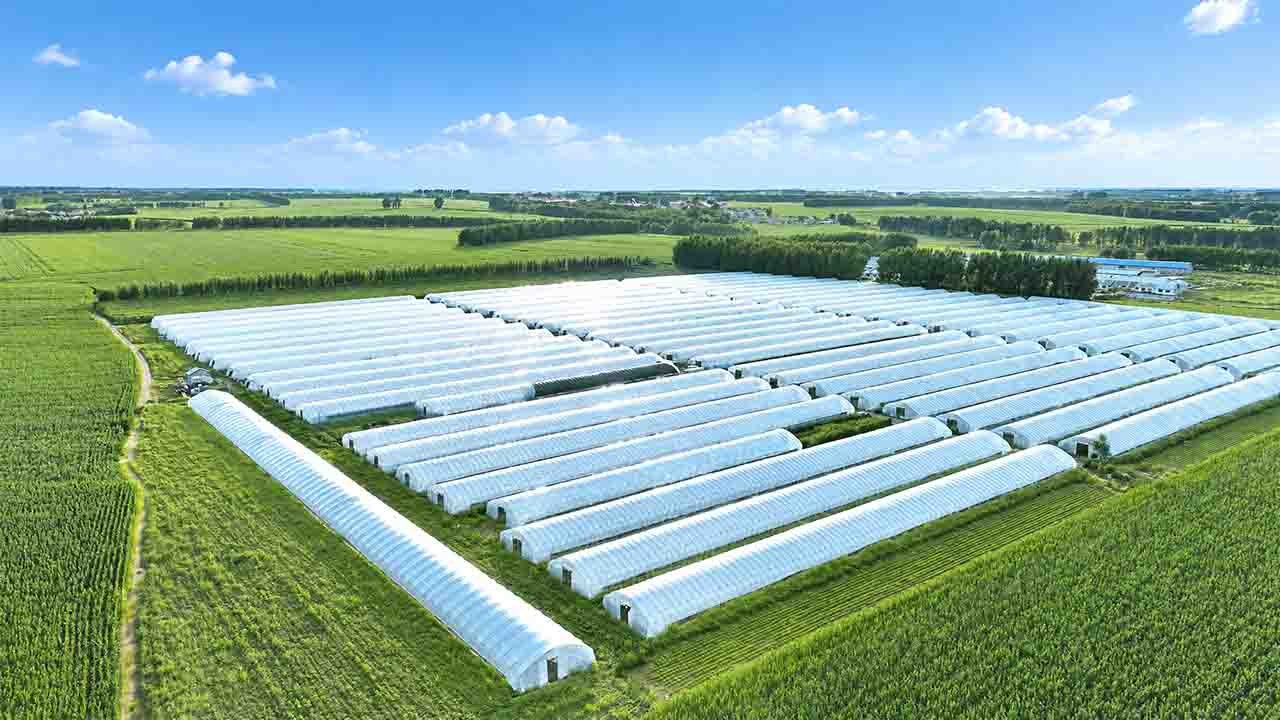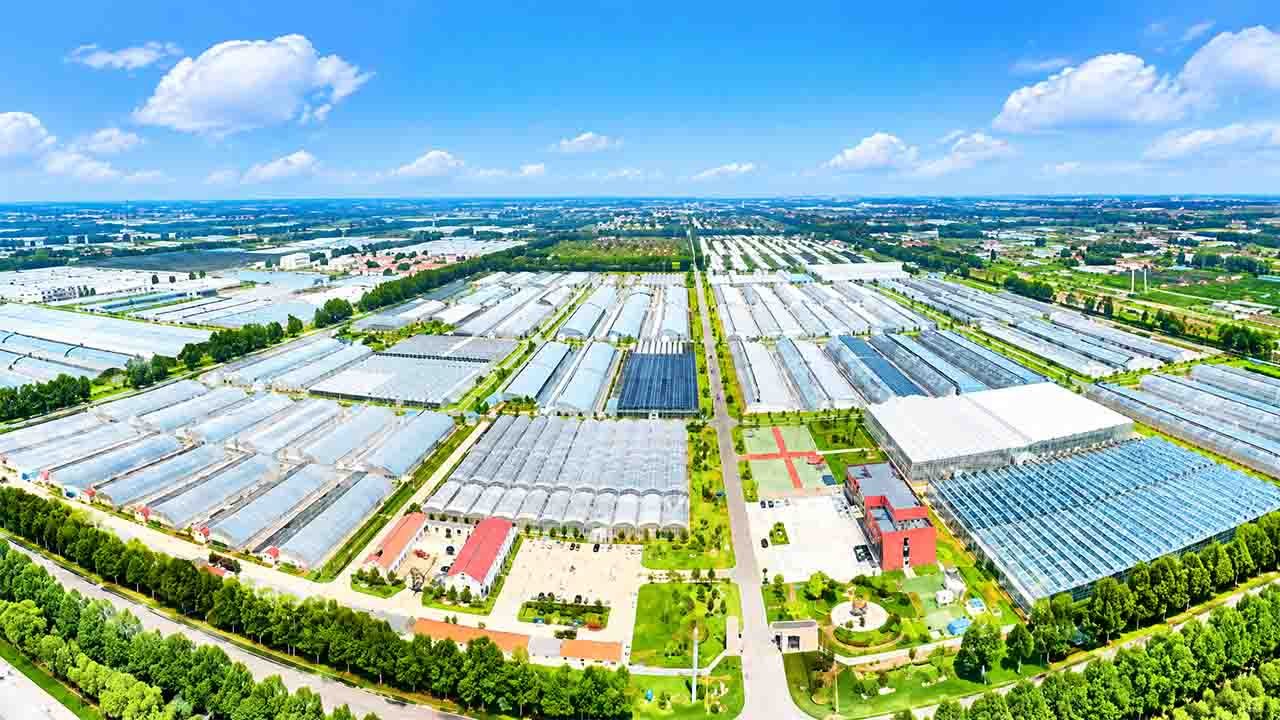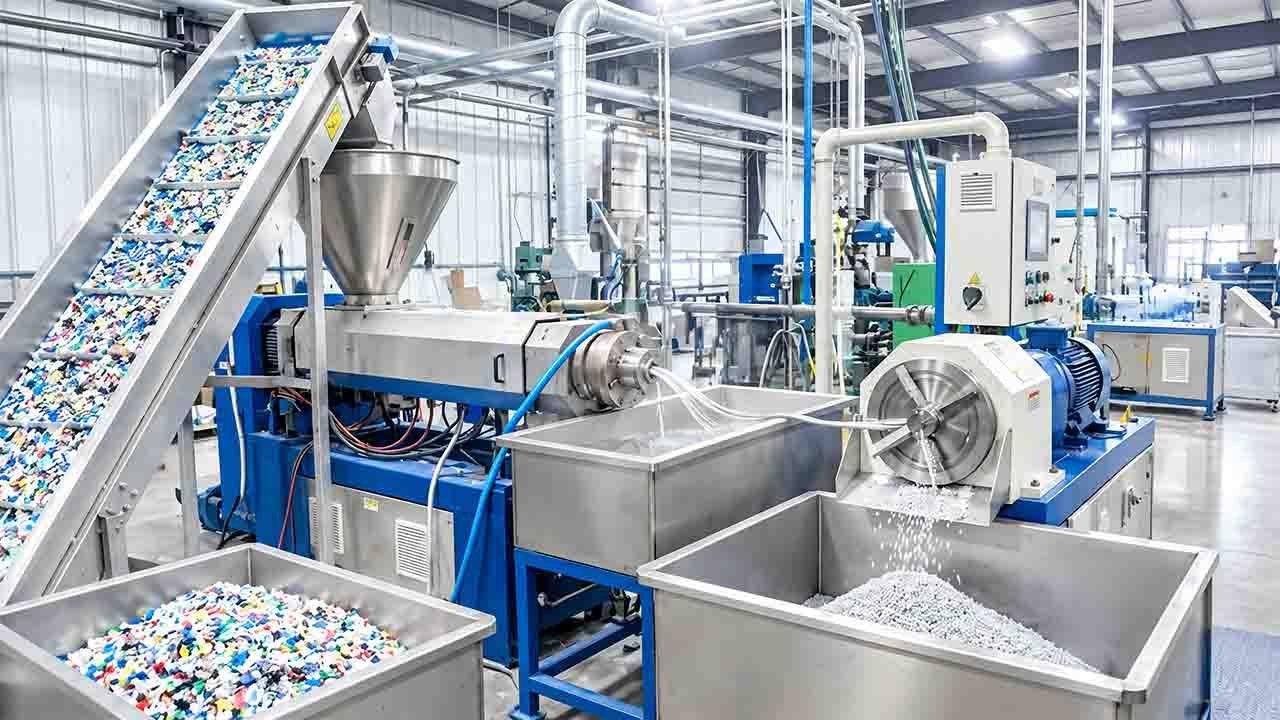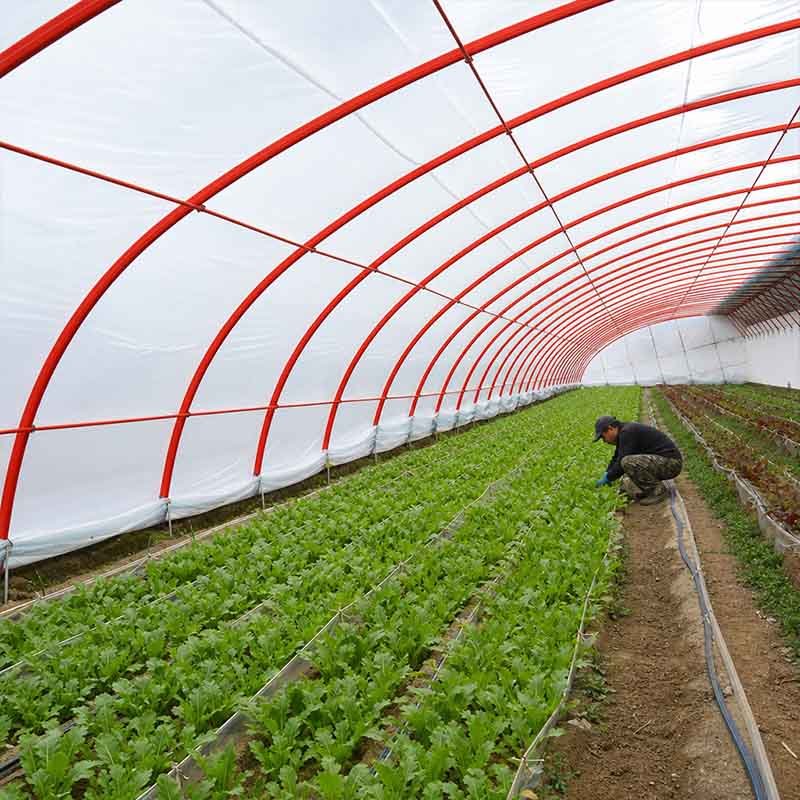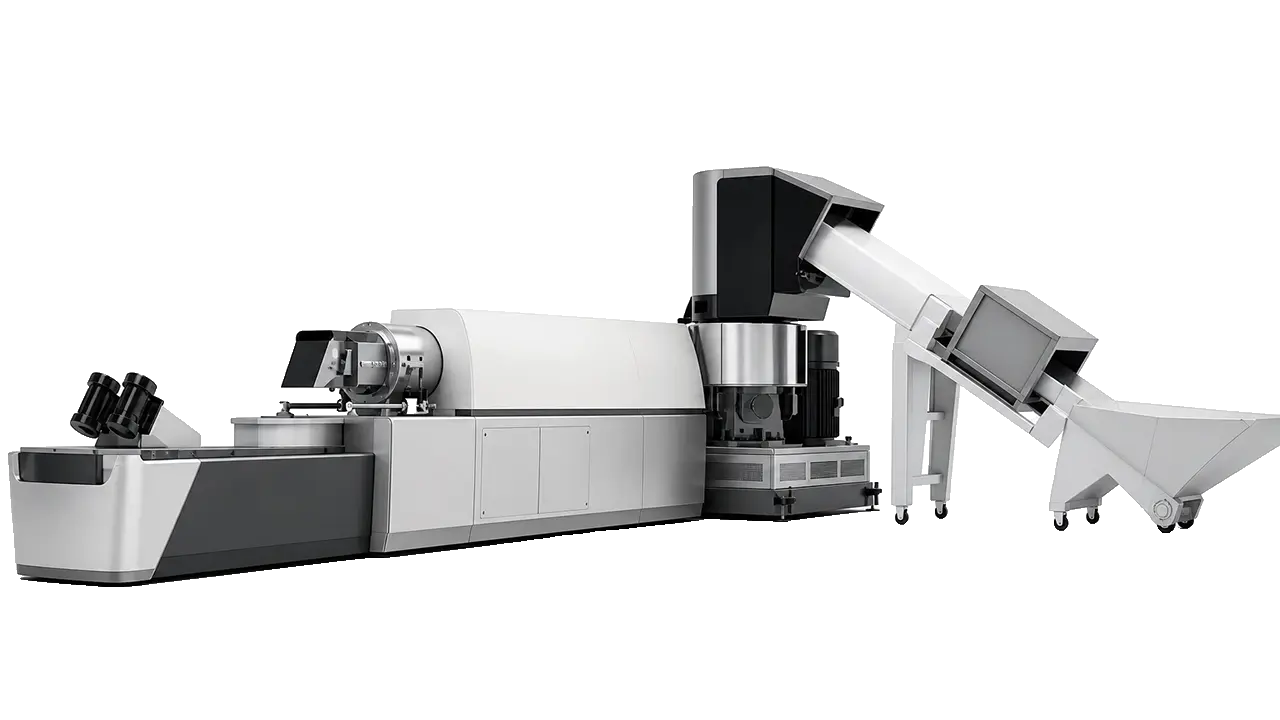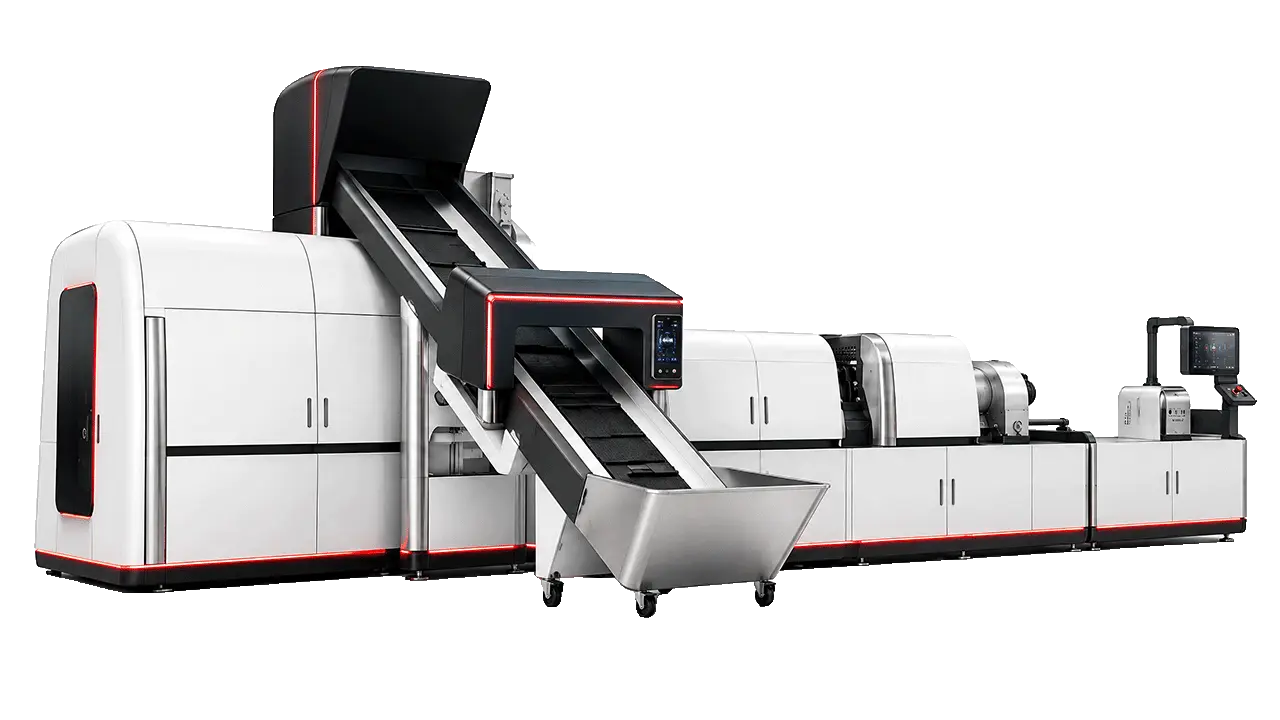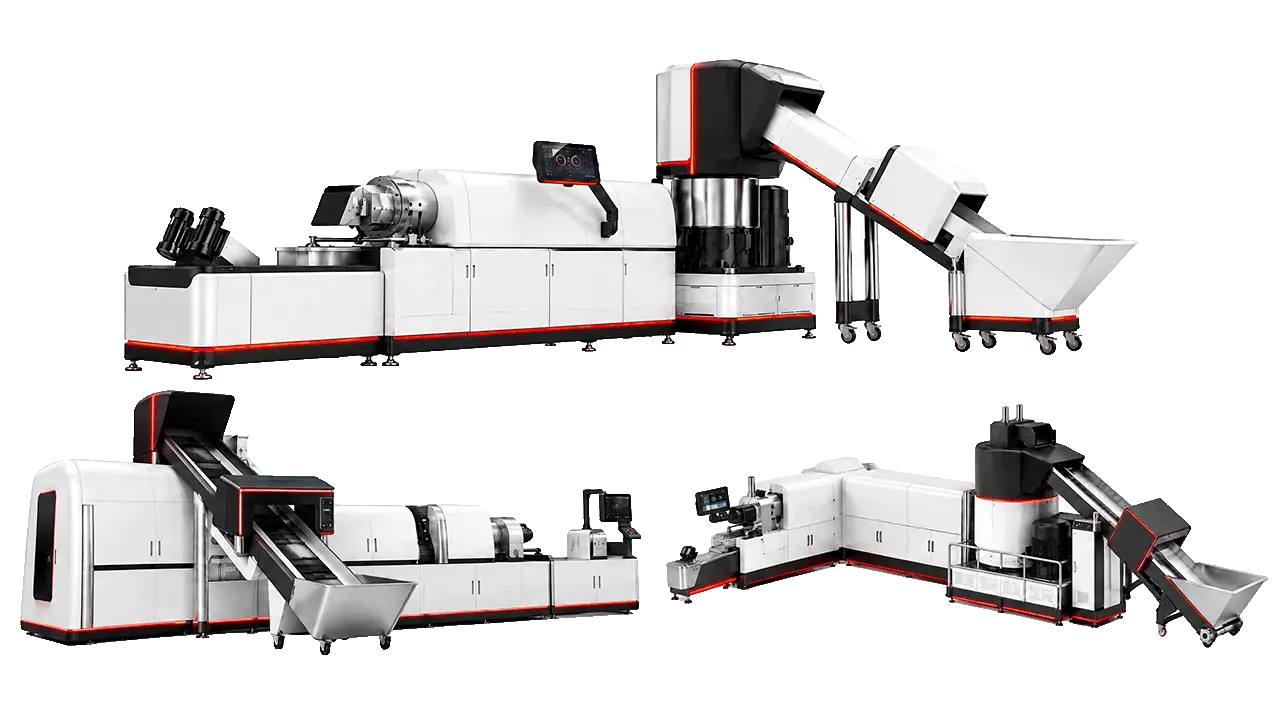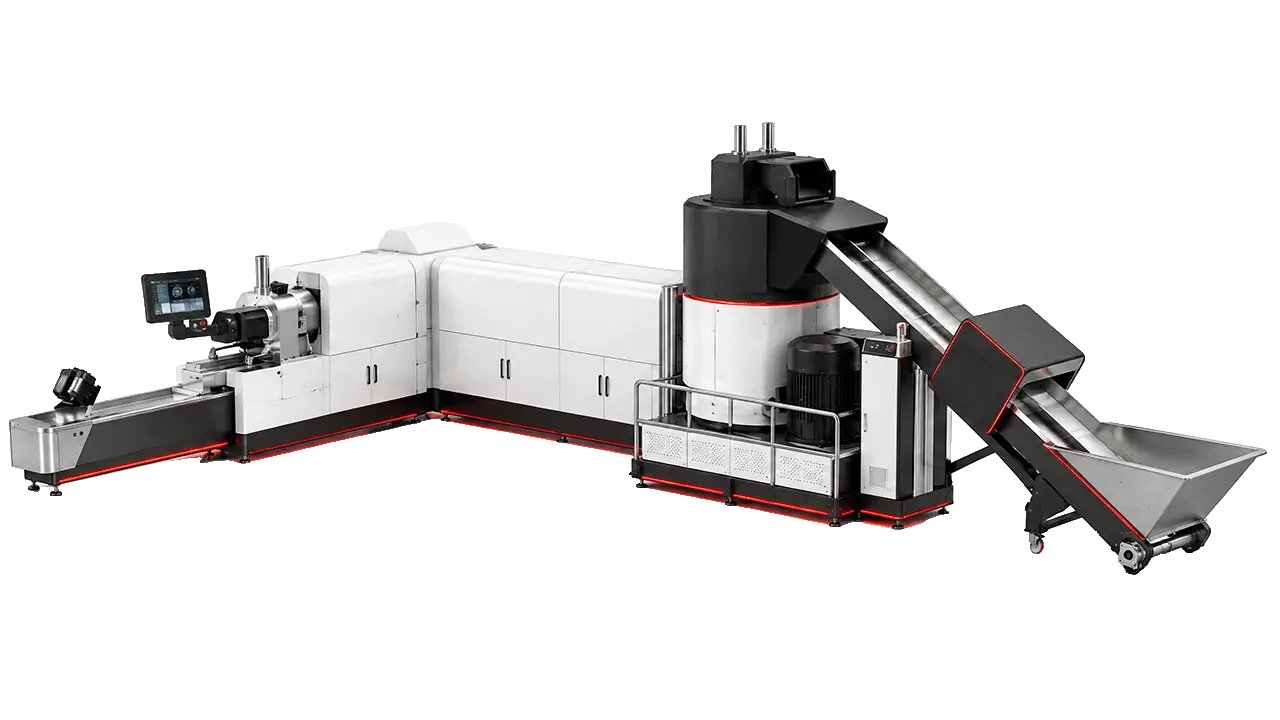
Engineered for the hardest plastic to recycle. Mulch film with 30–80% soil contamination, greenhouse film, silage wrap. Multi-stage wet washing, two-stage extrusion, water-ring pelletizing. 100–500 kg/h.
Agricultural film is not simply "dirty PE film." It is a fundamentally different input material — and understanding why determines whether your recycling project succeeds or fails.
Industrial PE film offcuts carry 5–15% contamination. Post-consumer PP woven bags: 10–30%. Field-collected mulch film carries 30–80% soil, sand and organic residue — the highest of any recyclable plastic stream.
Agricultural film collected from the field has an extremely low bulk density of 15–30 kg/m³. Standard screw feeders cannot maintain consistent throughput at this density. A dedicated compactor or forced-feeding unit is required — without it, the extruder starves.
Industrial waste has stable, predictable contamination. Agricultural film does not. The same region can produce mulch film with 3× more soil in the dry season than the wet season. Equipment must be sized for peak contamination, not average — and the process must include incoming material testing before sizing any line.
Agricultural film is among the most technically challenging plastic streams to recycle mechanically. Published research from Washington State University (2024) documents surface contamination ratios of 30–80% on field-recovered mulch film, primarily soil and plant debris — far exceeding the contamination levels of industrial PE film waste. This contamination profile requires purpose-built multi-stage wet washing systems. LayerQuestar Machinery agricultural film recycling lines are configured from the ground up for high-contamination input: dry pre-cleaning before the water loop, high-speed friction washing, float-sink separation, optional hot-wash for pesticide-laden material, and dual-stage dewatering to achieve ≤1% moisture before extrusion.
Agricultural film recycling serves three fundamentally different business models. The right equipment configuration depends on which scenario you are in — not just on throughput.
You generate your own greenhouse or tunnel film waste and want to process it on-site to reduce disposal costs and recover value.
You are running a regional agricultural film collection program, processing mixed farm film centrally to meet environmental compliance targets.
You purchase mixed farm film from multiple sources, process it into rLDPE pellets, and sell to downstream converters. Margin depends on the spread between input cost and pellet price.
Not sure which scenario fits your situation? That is normal — many agricultural film recycling projects start without a clear picture of their waste supply structure. Send us your film type, target daily volume and location → LayerQuestar Machinery's engineering team will help you assess feasibility before you commit to a configuration.
Every step below is present in a full agricultural film recycling line. The notes explain why agricultural film requires each step when other plastic streams do not.
Identify prohibited loads. Open bales under controlled conditions.
Remove loose soil, sand and stones before the material enters the water loop.
Reduce large film sheets to a consistent, washable flake size.
Initial water rinse. Heavy contaminants — stones, sand, metal fragments — sink and are removed early.
Fast-rotating paddles scrub film surfaces, releasing adhered soil and fine organic particles through a screened cylinder.
Density-based separation. LDPE/LLDPE (specific gravity <1.0) floats. Sand, soil, glass and denser polymers sink.
Heated water (and optional mild detergent) removes pesticide residues, oils and stubborn organic contamination.
Two-stage moisture removal. Centrifugal spin removes free water. Hot-air pipe drying reduces residual surface moisture.
Pre-compacts low-bulk-density film flakes before the extruder throat.
First stage melts and homogenises. Second stage degasses and builds pressure for filtration and pelletizing.
Removes residual solid particles from the melt without stopping the line.
Die-face cutting in water produces uniform cylindrical pellets. Vibrating screen removes fines and oversized particles. Pellets conveyed to storage silo.
Wet washing produces wastewater. This is not a footnote — it is a site qualification requirement. Confirm these conditions before selecting a location.
This wastewater cannot be discharged directly in most jurisdictions. Industrial wastewater discharge standards apply in China (GB 8978), the EU (Industrial Emissions Directive), and most Southeast Asian, South Asian and Latin American markets.
Wastewater is treated by sedimentation and filtration, then recirculated. Only evaporation losses are topped up with fresh water. This is the recommended configuration for sites with limited water supply or strict discharge limits.
LayerQuestar Machinery standard configuration can include a closed-loop water treatment module.
Wastewater passes through settling tanks to remove suspended solids, then is discharged under a local environmental permit. Requires approval from local environmental authority before construction.
Confirm local discharge standards for suspended solids and pesticide residues before selecting this path.
If the facility is located within an industrial park with centralised wastewater treatment, connection to the park system may be possible. Confirm the park accepts this wastewater category before committing to the site.
Understanding your pellet market before you build is as important as selecting the right equipment. rLDPE pellets from agricultural film have specific characteristics that determine which applications will accept them.
rLDPE pellets from agricultural film recycling are not suitable for food-contact packaging due to trace pesticide residues and degradation additives in the original material. This is a material characteristic, not an equipment limitation. Knowing this upfront allows you to target the right downstream markets.
The largest and most accessible market for rLDPE from agricultural film. Black or dark-coloured bags conceal colour inconsistencies in recycled resin. MFI requirements are relatively tolerant. Global demand is large and consistent.
Some markets accept mulch film and greenhouse film with a defined percentage of post-consumer recycled (PCR) rLDPE content. Colour and transparency requirements are low. MFI consistency is important for stable blown film production.
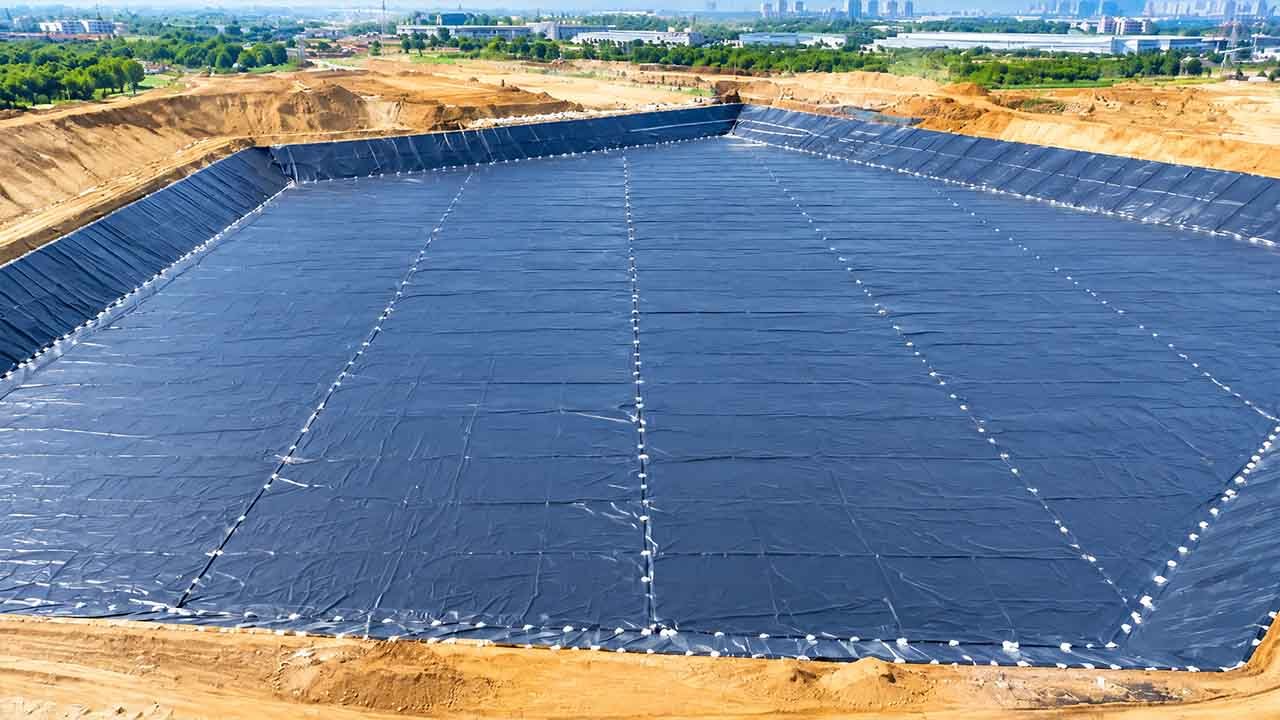
Waterproofing membranes, vapour barriers and geotechnical liners have no colour or transparency requirements. Tensile strength consistency matters. Both European and Asian markets have established demand.
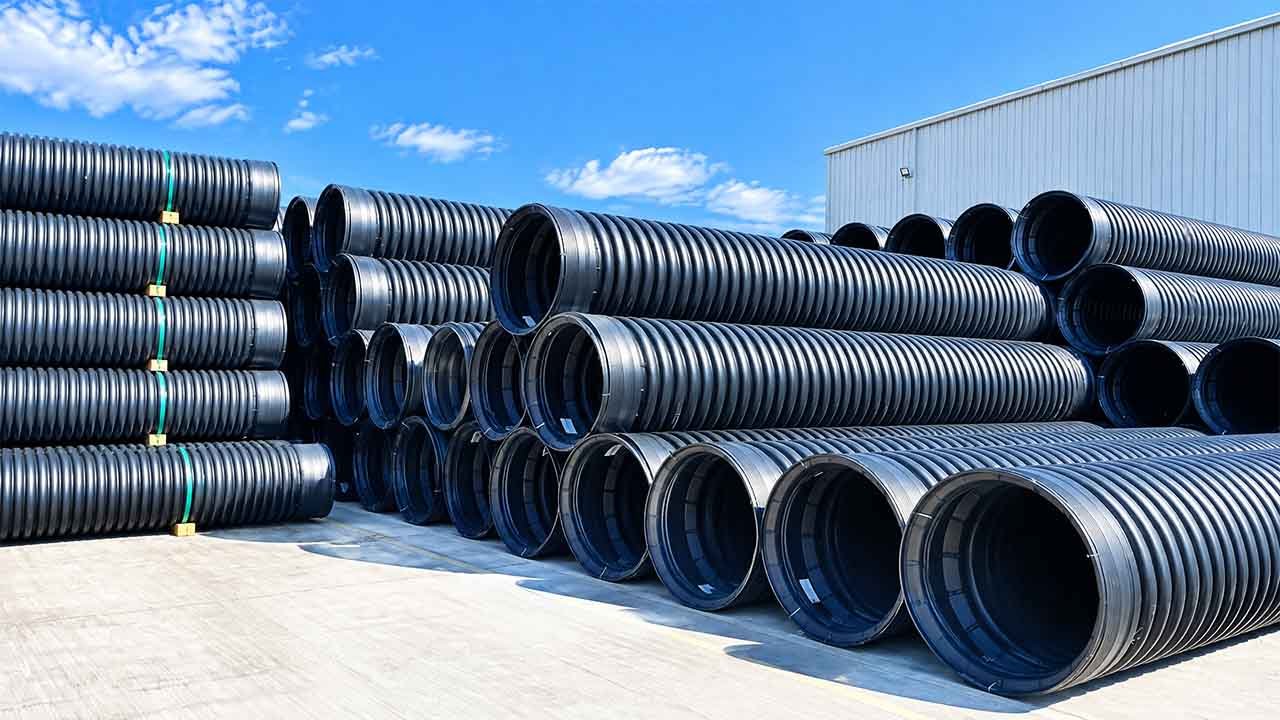
Irrigation drainage pipe, cable conduit and low-grade profiles accept rLDPE with lower purity requirements. Pellet quality requirements are the most tolerant of the four application categories.
| Factor | Effect on Pellet Quality | LayerQuestar Configuration |
|---|---|---|
| Incoming soil contamination level | Higher soil → higher ash content in pellet | Dry pre-cleaning + multi-stage wet wash |
| Moisture before extrusion | >1% → steam voids inside pellets | Dual-stage dewatering, target ≤1% |
| Melt filtration precision | Residual solids → surface defects, MFI instability | Continuous screen changer + fine filter |
| Vacuum degassing effectiveness | Residual VOCs + moisture → odour, voids | Two-stage extrusion, minimum 2 degassing zones |
| Pelletizing consistency | Irregular pellet size → downstream feeding problems | Water-ring die-face cutting with temperature control |
MFI reference range: Typical rLDPE pellets produced from agricultural film recycling lines fall within a MFI range determined by incoming material grade and processing conditions. Contact LayerQuestar Machinery for material-specific output data.
Two standard configurations. Final parameters — screw diameter, installed power and footprint — are confirmed by LayerQuestar Machinery engineering after incoming material assessment.
| Parameter | Standard Configuration Greenhouse / Tunnel / Silage Film |
Heavy Contamination Configuration Mulch Film / Mixed Farm Film |
|---|---|---|
| Applicable waste | Greenhouse film, tunnel film, silage wrap | Mulch film, mixed field waste |
| Capacity | 100–300 kg/h | 200–500 kg/h |
| Incoming contamination | ≤40% | 40–80% |
| Dry pre-cleaning | Trommel screen | Trommel screen (heavy-duty) |
| Washing system | Friction washer + float-sink tank | Friction washer + float-sink tank + hot-wash unit |
| Dewatering system | Centrifugal dryer + hot-air drying | Centrifugal dryer + mechanical press + hot-air drying |
| Moisture target (pre-extruder) | ≤1% | ≤1% |
| Extrusion stages | Two-stage | Two-stage |
| Vacuum degassing zones | Minimum 2 | Minimum 2 |
| Screen changer | Continuous (non-stop) | Continuous + secondary fine filter |
| Pelletizing method | Water-ring die-face cutting | Water-ring die-face cutting |
| Main motor brand | ABB preferred; Innomotics available | ABB preferred; Innomotics available |
| Temperature control | OMRON PID, ±1°C | OMRON PID, ±1°C |
| Water management | Closed-loop recycling (optional) | Closed-loop recycling (standard) |
| Factory acceptance test | 72-hr continuous run | 72-hr continuous run |
| Screw diameter / installed power / footprint | Confirmed by engineering after incoming material assessment | |
Every agricultural film recycling line ships after a 72-hour continuous factory acceptance test. Five hardware specifications that determine long-term reliability under high-contamination operating conditions.
Every line runs continuously for 72 hours at LayerQuestar Machinery's Zhejiang facility before shipment. The test verifies throughput consistency, temperature stability across all zones, screen changer function under load, pellet size uniformity and control system operation. No line ships without a completed FAT record.
For agricultural film lines, the FAT also verifies that the closed-loop water system maintains separation tank water quality over extended operation — a critical parameter that cannot be validated in a short-run test.
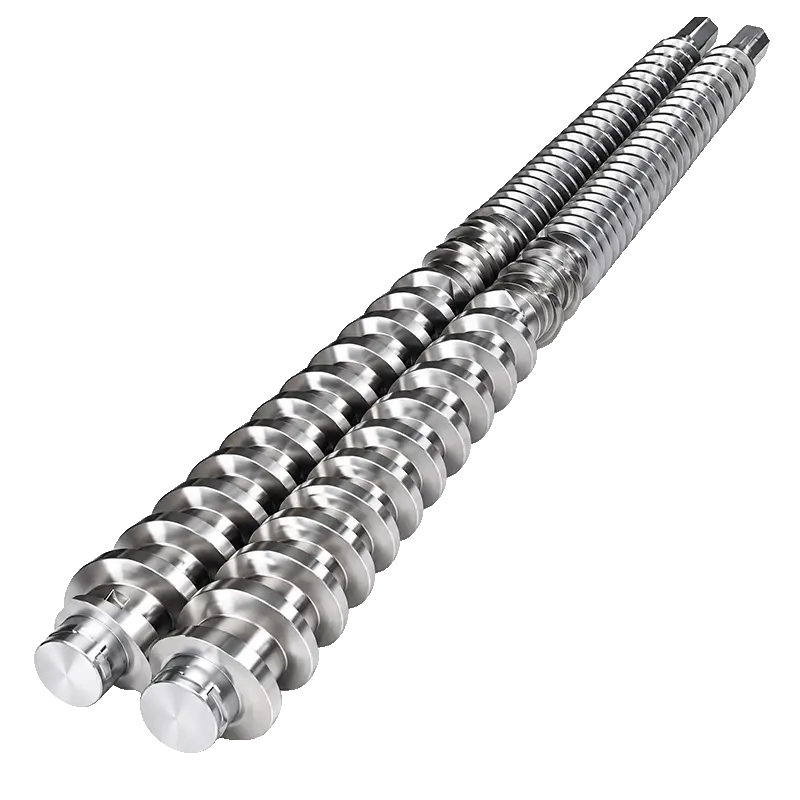
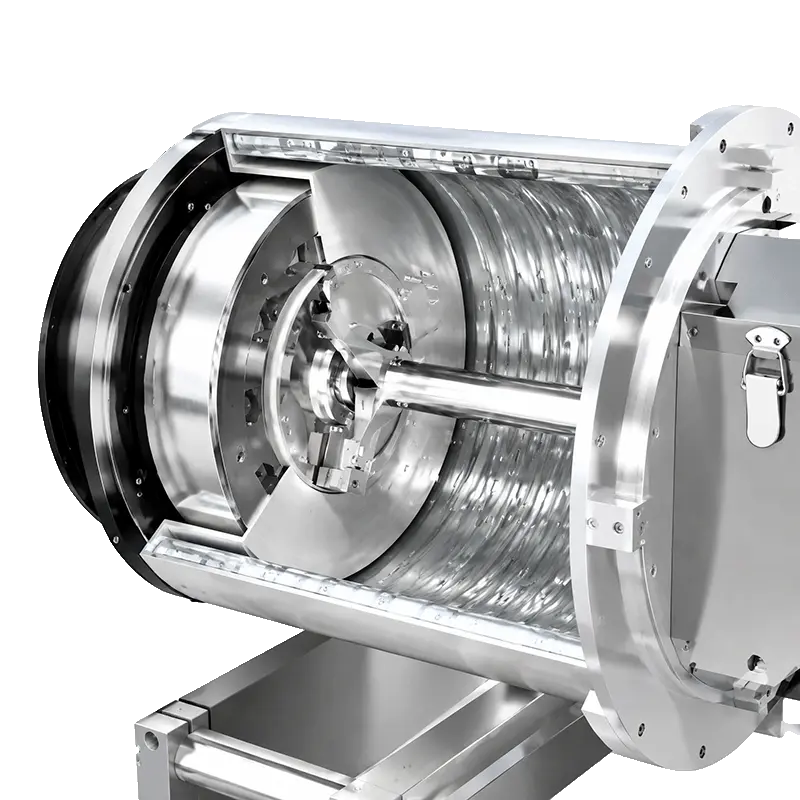
Base material: 38CrMoAlA nitrided steel. Surface: 1.5–3mm tungsten carbide alloy overlay. Hardness: HRC 59–65. Designed for continuous operation against the abrasive sand and inorganic particles present in agricultural film melt streams.
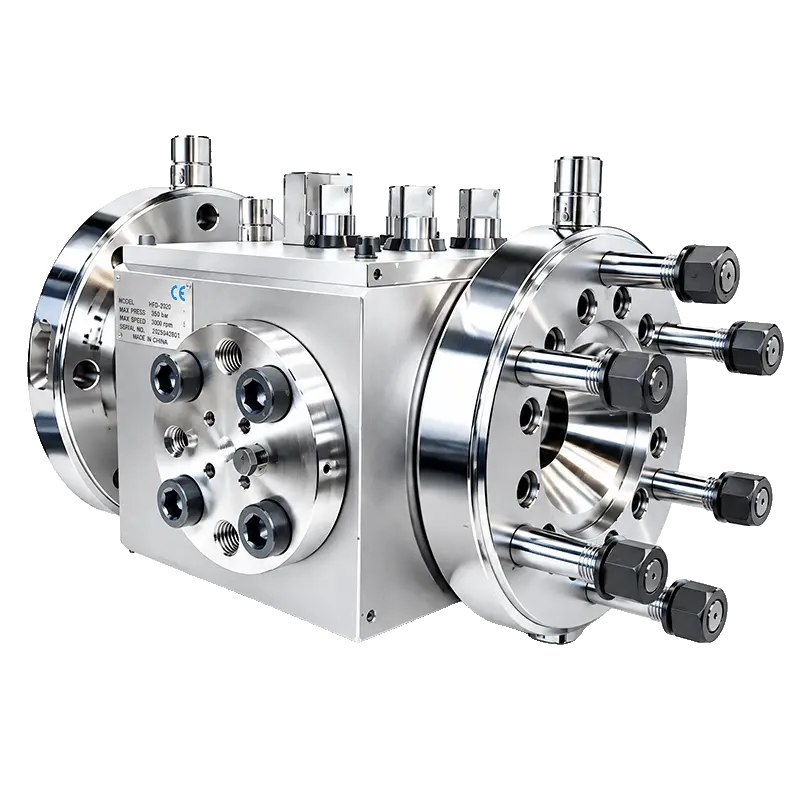
Non-stop screen replacement under full production pressure. Agricultural film melt contains significantly more residual inorganic particles than industrial film — screen change frequency is higher. A manual screen changer would require repeated production stops. The continuous design eliminates this downtime.
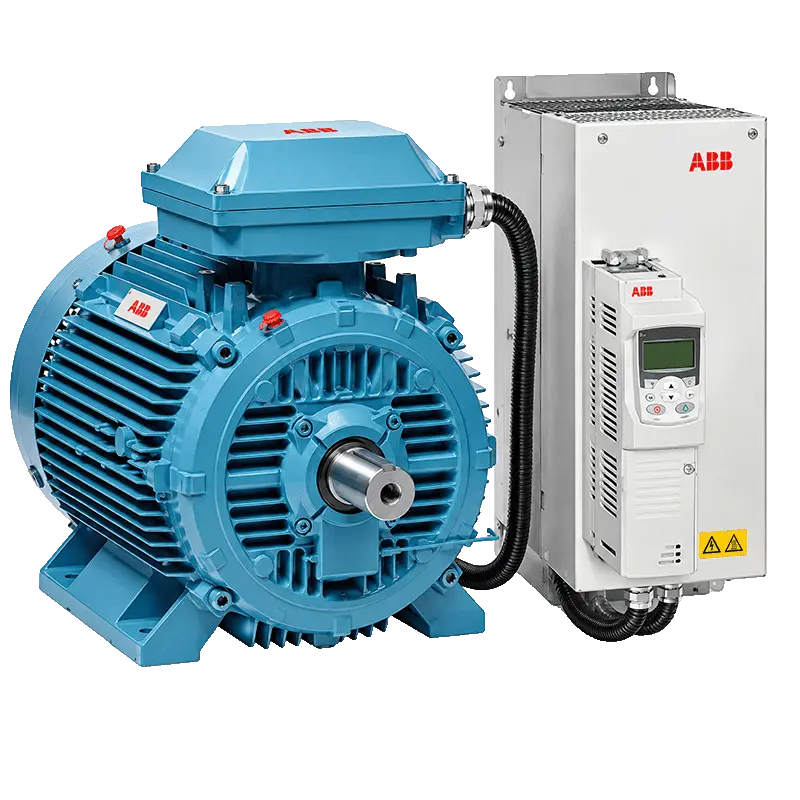
ABB motors are the preferred specification. Innomotics and other international brands are available on request. International-brand motors are specified because spare parts and service are available in LayerQuestar's 120+ export markets — not just in China.
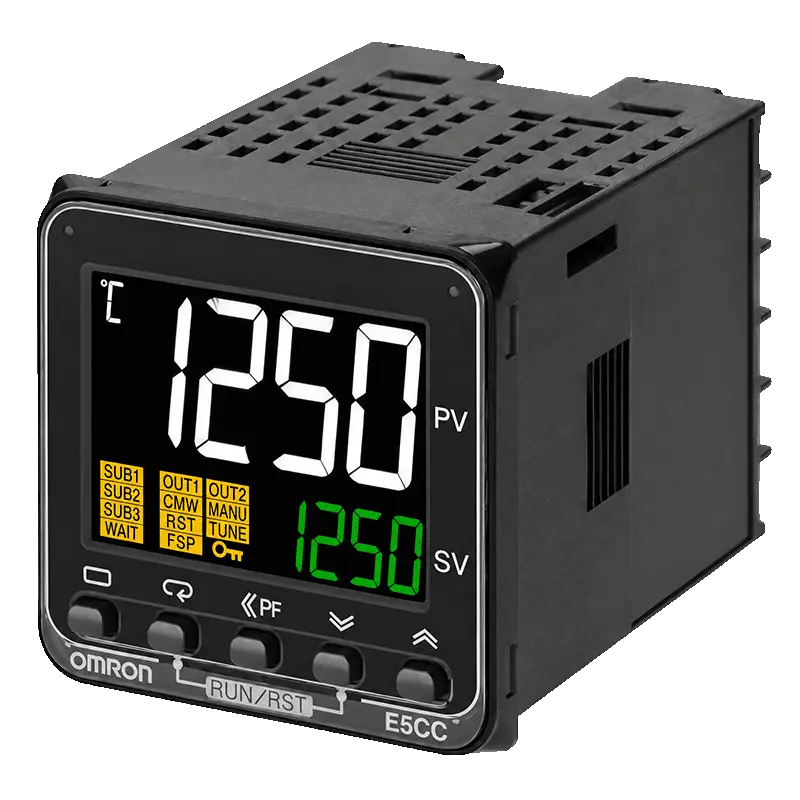
OMRON PID controllers on every heating zone. Deviation ±1°C under stable operating conditions. Independent zone control across both extrusion stages. All control cabinet labels are in English. Two to three independent cooling fans per cabinet.
Die-face cutting in a water ring produces uniform, dense cylindrical pellets suited to LDPE's low melting point. Pellet size is controlled by die hole diameter and cutter speed. Output passes through a vibrating screen to remove fines before the storage silo.
Agricultural film recycling lines operate in demanding conditions. Wear parts consume faster than in industrial film applications. Spare parts availability is not a secondary consideration.
Standard warranty terms apply to all LayerQuestar Machinery agricultural film recycling lines. Warranty scope and duration are confirmed in the supply contract.
Agricultural film lines consume wear parts at higher rates than industrial film lines due to abrasive input. Critical wear parts stocked and available from Zhejiang:
Remote diagnostic support via video call and PLC data review. All control cabinets are fully English-labelled. Operation and maintenance manuals supplied in English. On-site commissioning support available — confirm scope and schedule at order stage.
These are the questions that determine whether an agricultural film recycling project is viable — not just how the equipment works.
It depends on four variables: the cost of acquiring waste film, the cost of processing (energy, water, labour, wear parts), the selling price of rLDPE pellets in your local market, and whether government subsidies or plastic bag ban compliance incentives apply in your region.
Agricultural film recycling is commercially viable in markets where at least one of the following conditions is true: (1) waste film collection cost is low because the source is concentrated and accessible; (2) rLDPE pellet prices are supported by local demand for garbage bags, construction film or agricultural film with PCR content; or (3) government subsidies or compliance requirements offset processing costs.
Before committing to equipment, map your specific input cost, processing cost and pellet price. LayerQuestar Machinery can provide processing parameter data to support your financial model — but the commercial viability assessment must be done with local market data.
rLDPE pellets from agricultural film are not suitable for food-contact packaging due to trace pesticide residues and degradation additives. The main downstream applications are: garbage bags (the largest market — dark colour conceals resin inconsistencies), new agricultural film with PCR content, construction waterproofing membranes and geomembranes, and non-pressure irrigation pipe and drainage profiles.
Pellet quality — determined by washing thoroughness, moisture control and filtration precision — determines which of these applications will accept your material. Higher-quality pellets open more markets and command better prices.
Yes. Wet washing produces wastewater containing suspended solids, organic matter and, in the case of mulch film, potential pesticide residues. Direct discharge is not permitted in most jurisdictions. You need either a closed-loop water recycling system (recommended), a sedimentation and permitted discharge system, or access to an industrial park centralised treatment facility.
The closed-loop water recycling module is the most practical solution for most sites. It eliminates discharge permitting complexity and reduces fresh water consumption significantly. Confirm with LayerQuestar Machinery whether this module is included in your quoted configuration.
Yes — with the correct process configuration. The key is removing contamination at every stage before it reaches the extruder: dry pre-cleaning removes loose soil before the water loop; friction washing and float-sink separation remove the remainder; hot-wash handles pesticide residues; dual-stage dewatering brings moisture to ≤1%; and continuous filtration removes residual melt-phase particles.
The resulting pellets are suitable for garbage bags, agricultural film with PCR content, construction membranes and non-pressure pipe. They will not meet food-contact or transparent film specifications — but those are not the target markets for agricultural film recyclate.
No. Drip irrigation tape contains rigid plastic fittings (typically PP or ABS) and metal emitters. These cannot be separated from the film stream by the float-sink tank or screen changer. They damage shredder blades, block the screen changer and introduce contamination into the pellet. Drip tape requires a separate processing line with dedicated rigid-plastic separation. Contact LayerQuestar Machinery for a separate assessment if your waste stream includes drip tape.
LDPE and LLDPE are more sensitive to moisture during extrusion than PP. When moisture exceeds approximately 1%, water vaporises in the melt and forms steam bubbles. These bubbles create internal voids inside the pellets. Pellets with internal voids perform poorly in downstream blown film and stretch film applications — they cause bubble instability and film defects.
The ≤3% standard is used for PP woven bag recycling, where PP's higher processing temperature and different melt rheology make it more tolerant of residual moisture. Applying the PP standard to LDPE agricultural film recycling is a specification error that produces lower-quality pellets.
A closed-loop water recycling system significantly reduces fresh water consumption by recirculating wash water after treatment — only evaporation losses need to be topped up. This makes wet-wash lines viable in water-constrained locations that would not support a once-through water system.
However, a minimum reliable water source is still required for initial fill and top-up. If your site has genuinely no water access, contact LayerQuestar Machinery to discuss whether a dry pre-cleaning configuration can address your specific waste stream — noting that dry-only processing has significant limitations for high-contamination agricultural film.
This is a real operational planning question. Three approaches are used in practice: (1) stockpile baled film during peak collection season and process year-round; (2) supplement with other PE film streams — greenhouse film, industrial stretch film, or post-consumer PE bags — during the agricultural off-season; (3) accept seasonal operation and plan maintenance and overhaul during the downtime period.
Option 2 is the most common for commercial recyclers. The LayerQuestar Machinery agricultural film line can process other clean-to-medium PE film streams in addition to agricultural film — confirm the specific input materials with our engineering team to verify compatibility.
The first step is not selecting equipment — it is validating your waste supply and your pellet market. Before contacting any equipment supplier, answer these four questions:
Once you have answers to these four questions, contact LayerQuestar Machinery with the details. We will recommend a specific line configuration and provide the technical parameters you need to complete your financial model.
The primary practical differences for buyers in developing and emerging markets are: lead time, spare parts availability and total cost of ownership. LayerQuestar Machinery ships from Zhejiang, China, with spare parts available globally through our network in 120+ countries. All control systems use internationally sourced components (OMRON, ABB) that are serviceable locally in most markets.
On process technology, the core washing and pelletizing steps are comparable. The LayerQuestar line uses WC bi-metallic screws (HRC 59–65), continuous screen changers and OMRON PID temperature control — specifications chosen for long-term reliability under the abrasive conditions of agricultural film processing. Every line completes a 72-hour factory acceptance test before shipment.
The viability of an agricultural film recycling project depends on four inputs: film type (mulch / greenhouse / silage), contamination level, target daily throughput, and site water conditions. Send LayerQuestar Machinery these four details and our engineering team will provide a specific system recommendation and the technical parameters you need to complete your investment assessment.