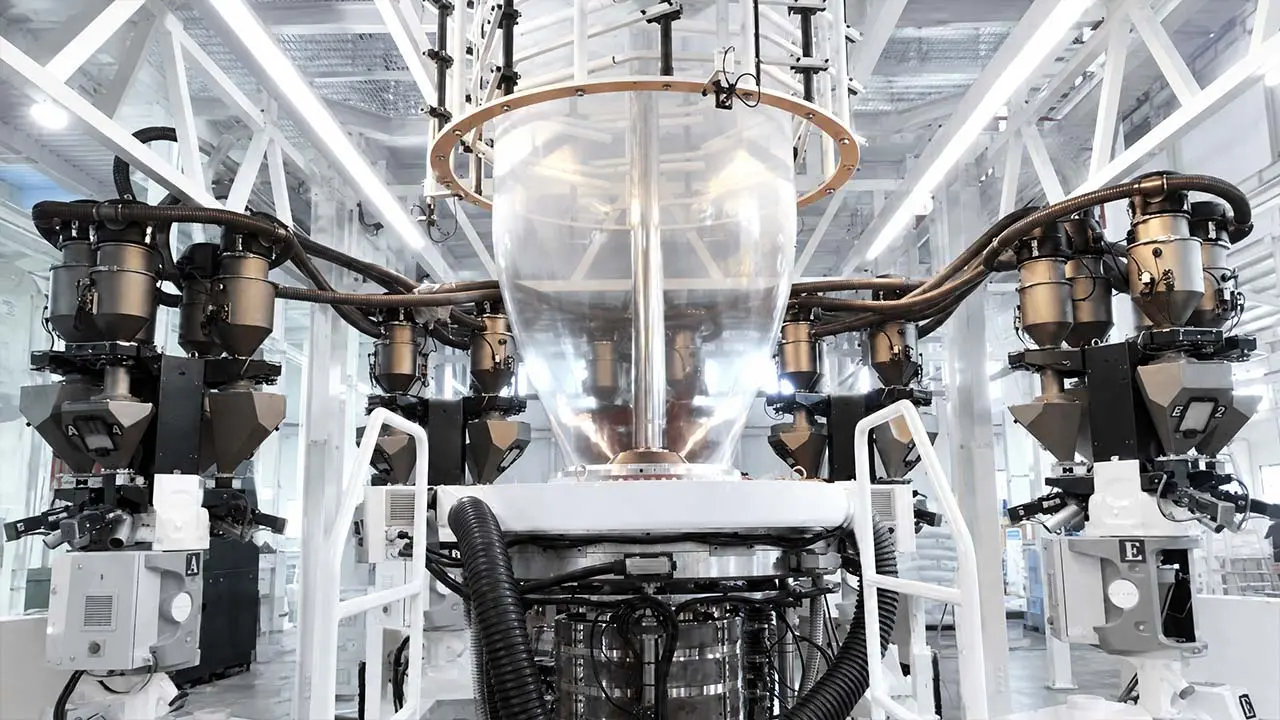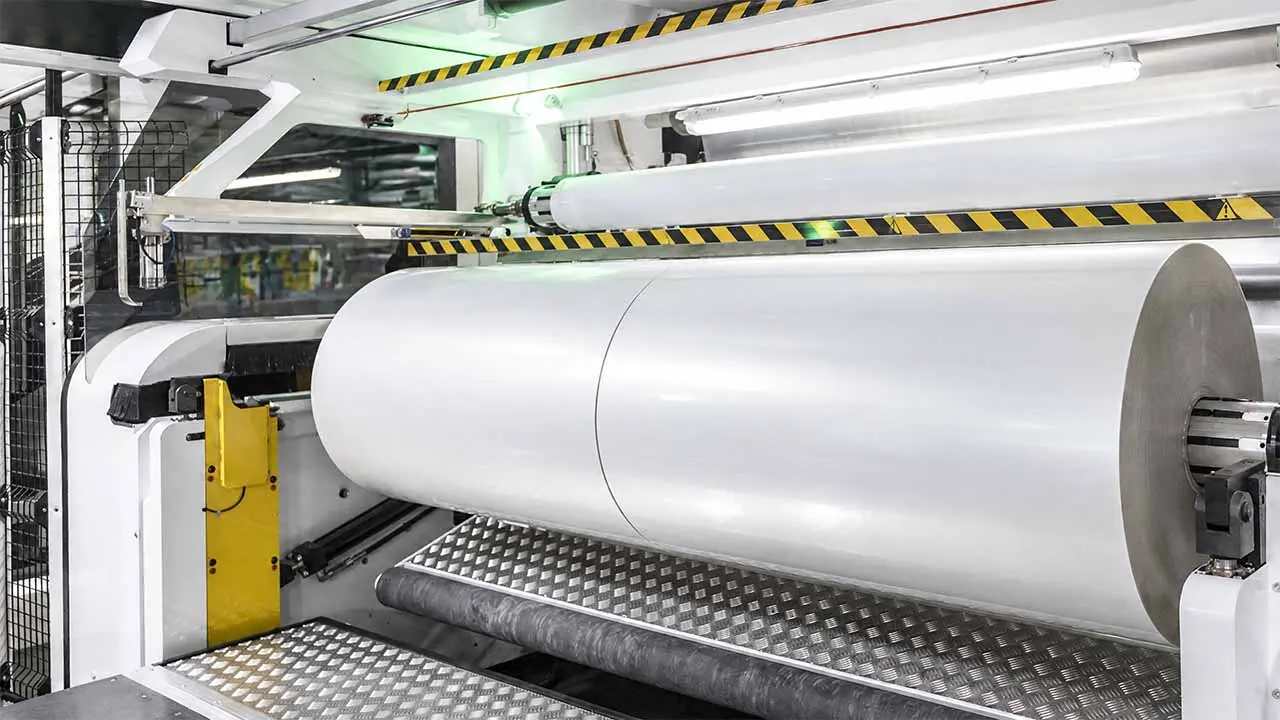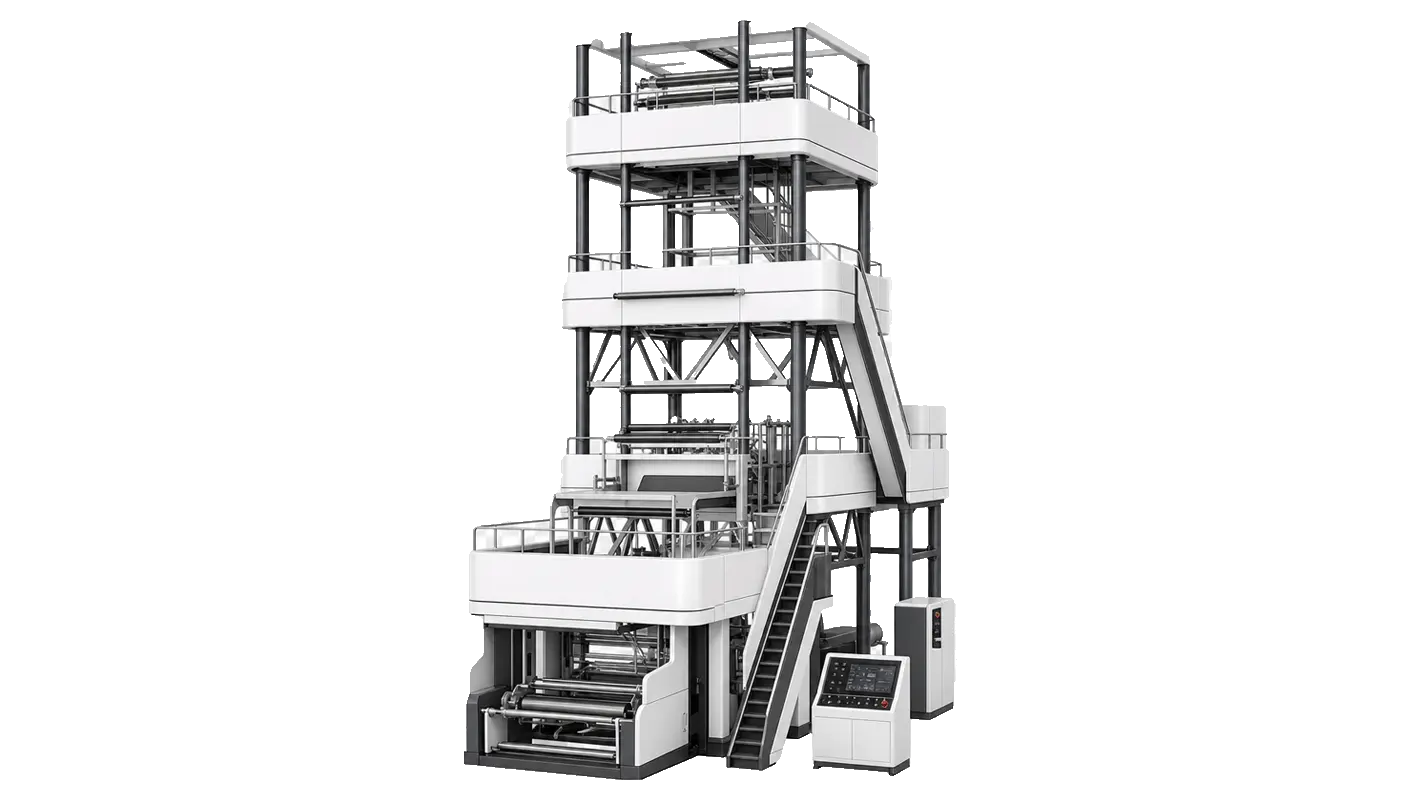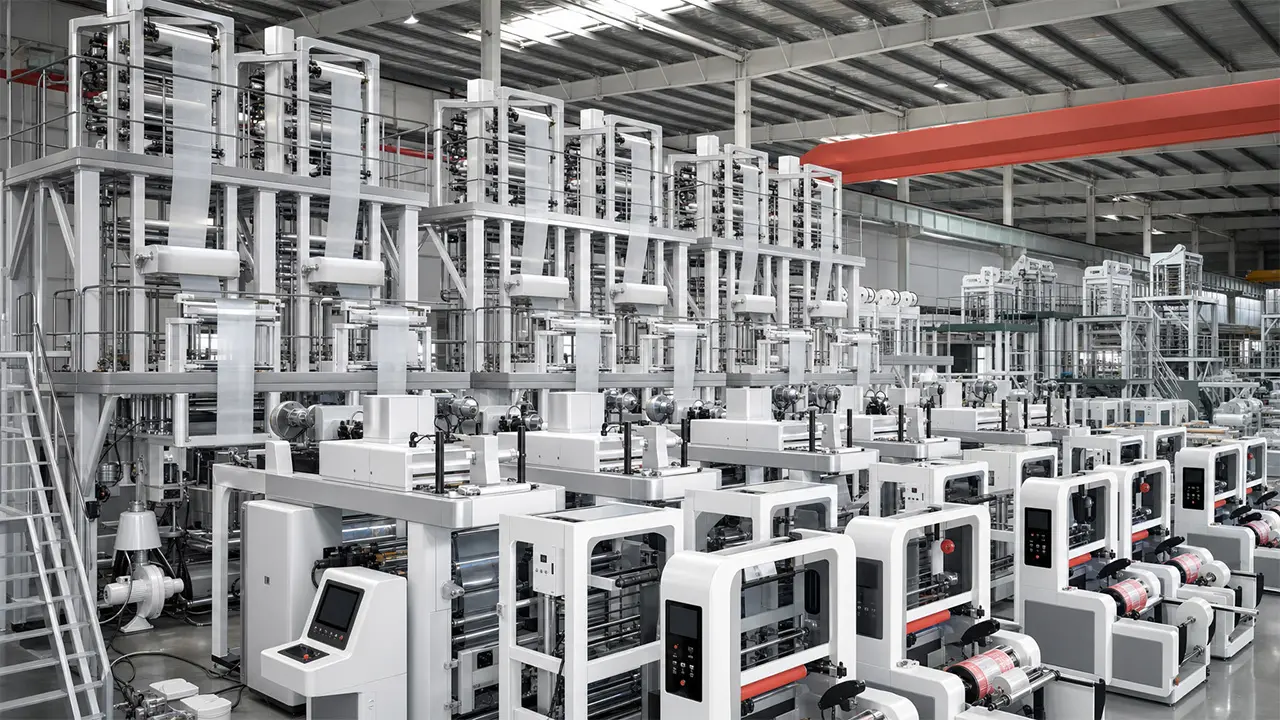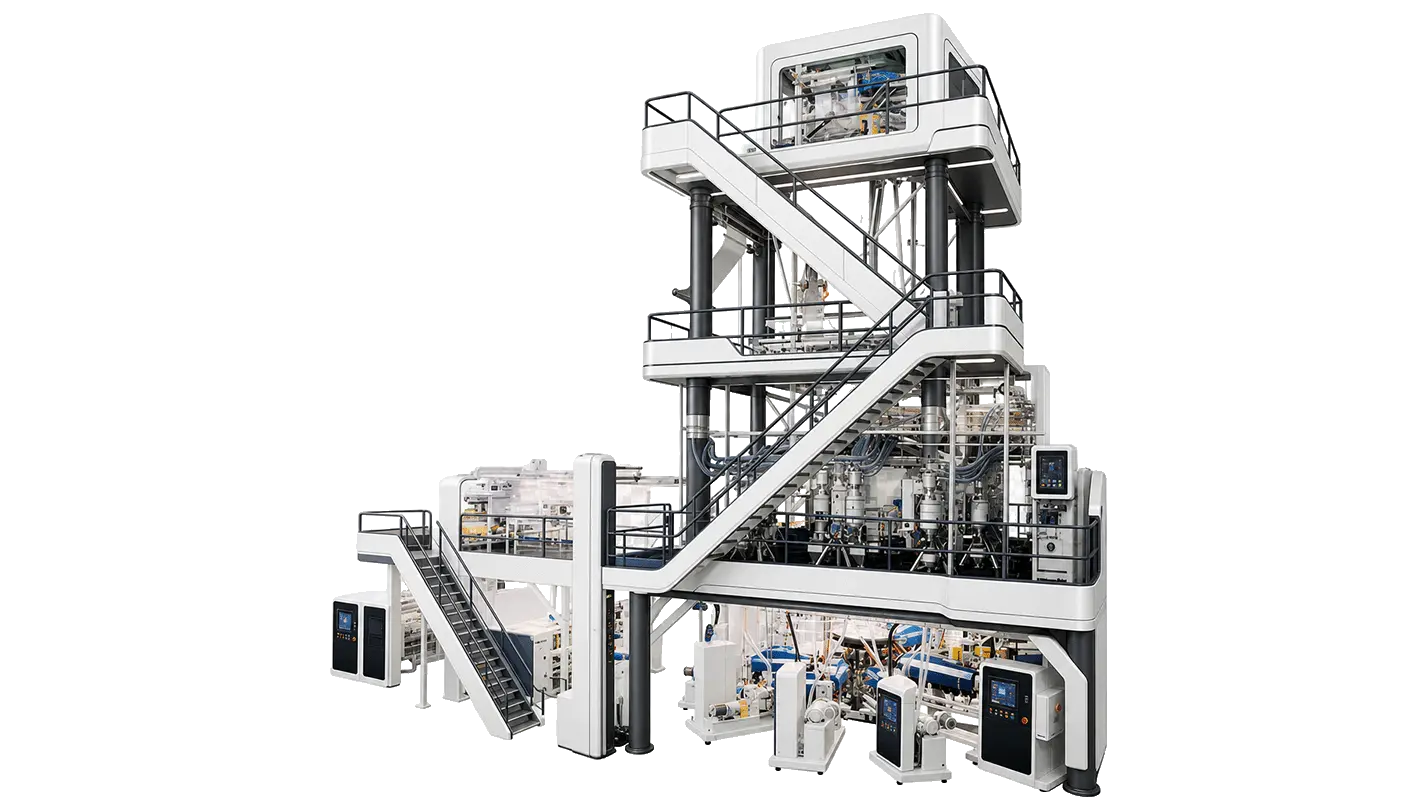
LayerQuestar 9-layer EVOH barrier co-extrusion blown film machine in operation
9 Layer · Dual-PE EVOH Barrier

9-Layer EVOH Barrier
Blown Film Machine

The highest-layer co-extrusion platform in the LayerQuestar range — dual PE outer and inner layers, PA nylon protection and an EVOH oxygen-barrier core in a single symmetric structure: PE / PE / TIE / PA / EVOH / PA / TIE / PE / PE. For ultra-long shelf-life food packaging, high-specification medical film and demanding industrial barrier applications.

9 Layers
5 Extruders
150–600kg/h Output Range
72hr Factory Run Test
Need full asymmetric control over every layer? A 9-extruder fully independent configuration is available on request — contact LayerQuestar to discuss your requirements.
Get a Configuration Proposal
Applications

What Does a 9-Layer EVOH Barrier Film Machine Produce?

A 9-layer co-extrusion blown film machine adds two independent PE structural layers on each side of the barrier core — separating surface performance from structural strength in a way no 7-layer machine can match. The result is film engineered for the most demanding shelf-life, puncture-resistance and surface-specification requirements.

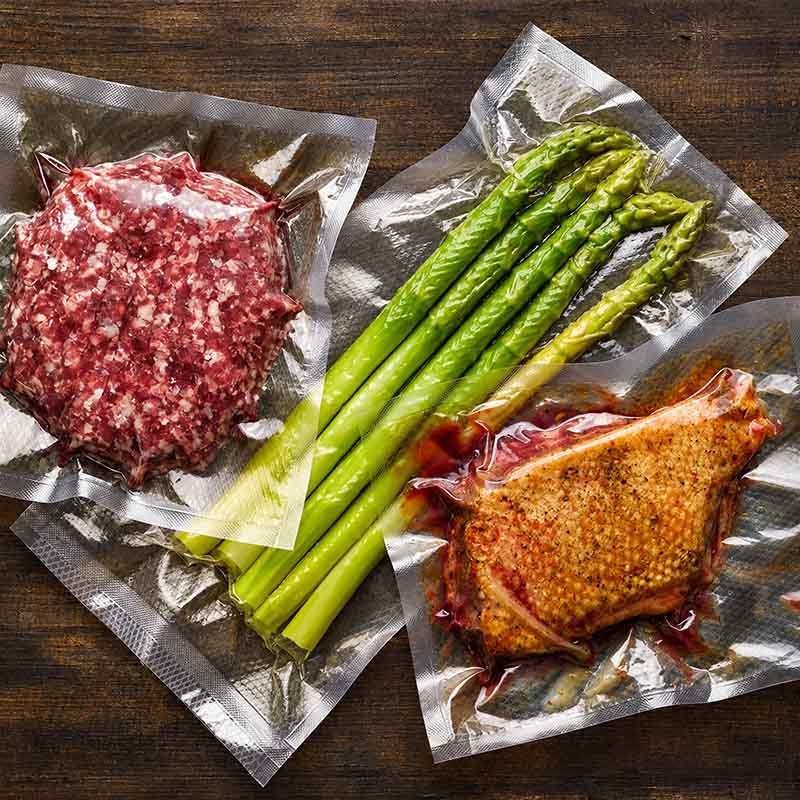
Ultra-long shelf-life vacuum-packed food products in 9-layer EVOH barrier film
Primary Application

Ultra-Long Shelf-Life Food Packaging

Ambient-stable processed meats, UHT dairy products, military rations and retort pouches requiring shelf life beyond 6 months without refrigeration. The dual-PA structure surrounding the EVOH core provides maximum protection against moisture ingress and mechanical stress during retort processing.

High-specification medical device and pharmaceutical packaging film from 9-layer blown film line
Primary Application

High-Specification Medical & Pharmaceutical Film

Implantable device packaging, long-term sterile storage pouches and pharmaceutical blister backing where both oxygen and moisture exclusion must be maintained over multi-year storage periods. The dual outer PE layers allow independent specification of print surface and structural layer without compromise.

Industrial ultra-high barrier film rolls for electronics and precision component packaging
Secondary Application

Industrial Ultra-High Barrier Film

Long-term moisture and corrosion protection for precision electronics, aerospace components and high-value instruments. The 9-layer structure provides the highest barrier performance available from a blown film platform, with the mechanical toughness to withstand demanding handling and storage conditions.

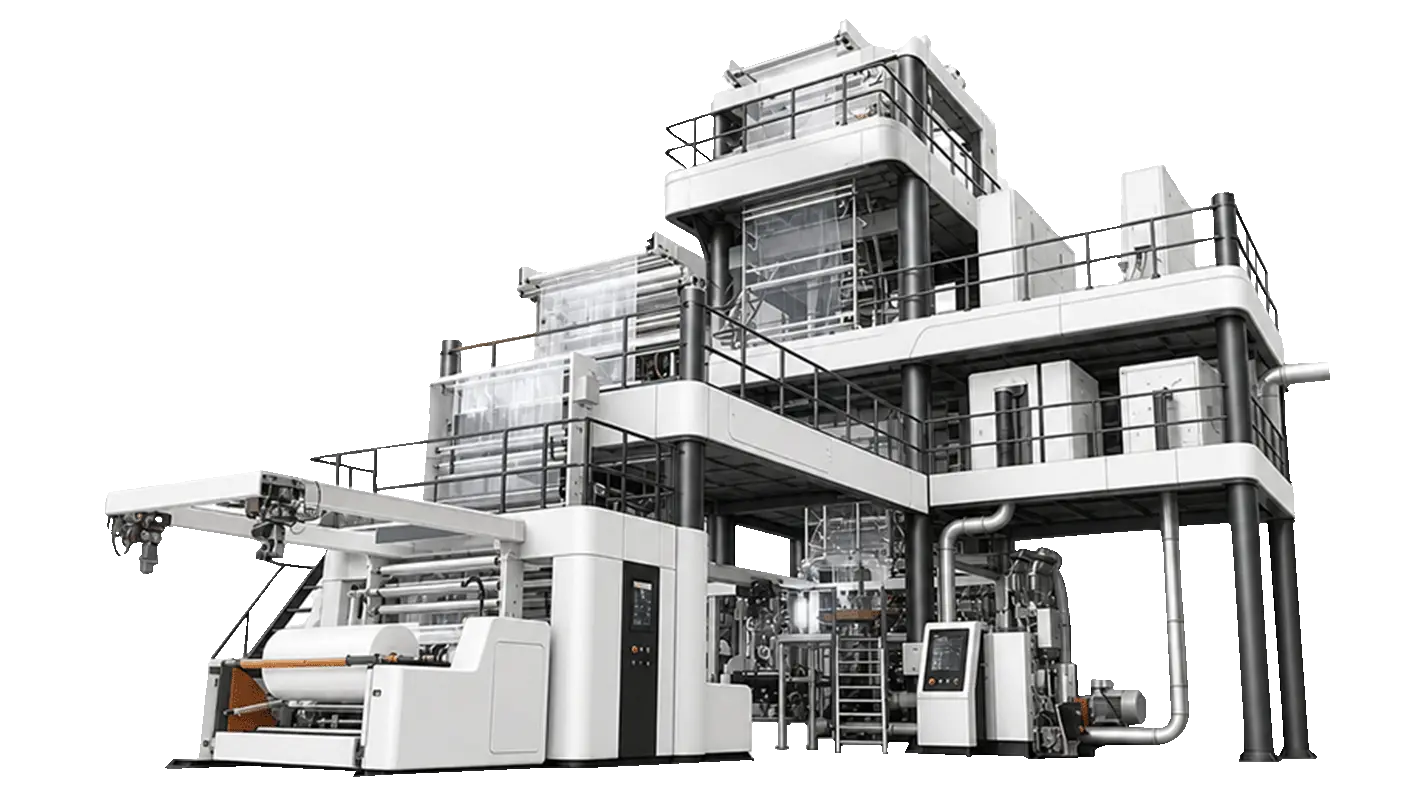
LayerQuestar Machinery's 9-layer co-extrusion blown film line is the top of the LayerQuestar barrier film range — specified when a 7-layer structure is not sufficient for the application's shelf-life, puncture-resistance or surface-specification requirements. The standard configuration uses 5 extruders with die-head flow splitting to produce the full 9-layer PE/PE/TIE/PA/EVOH/PA/TIE/PE/PE structure. A fully independent 9-extruder asymmetric configuration is available on request for applications requiring different material formulas in every layer.

Layer Architecture

9-Layer Film Structure Explained

Nine layers, five extruders. Understanding how die-head flow splitting produces a symmetric 9-layer structure — and why the dual PE layers on each side are the defining upgrade over a 7-layer machine.

Why 9 layers instead of 7? In a 7-layer structure, each outer PE layer must simultaneously handle printability, gloss and structural strength — a single layer doing two jobs. The 9-layer structure splits these functions: L1 is optimised purely for surface performance (print adhesion, gloss, slip), while L2 is optimised purely for structural strength (stiffness, puncture resistance, thickness). The inner side mirrors this logic. The result is a film where every layer does one job well, rather than two jobs acceptably.

Standard Configuration — Symmetric 5 Extruders · 9 Layers

LAYER EXTRUDER MATERIAL THICKNESS % FUNCTION L1 — PE outer-1 Ext A LDPE / LLDPE + slip / anti-block ~16% Print surface, gloss, anti-block L2 — PE outer-2 Ext B LLDPE / mLLDPE (structural) ~15% Structural strength, stiffness, gauge L3 — TIE Ext C Adhesive Tie Resin (maleic anhydride) ~8% Bonds PE-2 to PA — prevents delamination L4 — PA Ext D Nylon PA6 / PA6,66 ~10% Puncture resistance, protects EVOH outer side L5 — EVOH Core Ext E EVOH (32–44 mol% ethylene) ~9% Primary oxygen barrier — dedicated extruder, no splitting L6 — PA Ext D ↩ Nylon PA6 / PA6,66 ~10% Mirrors L4 — protects EVOH inner side L7 — TIE Ext C ↩ Adhesive Tie Resin (maleic anhydride) ~8% Bonds PA to inner PE-2 layer L8 — PE inner-2 Ext B ↩ LLDPE (structural, mirrors L2) ~15% Structural strength, flexibility, inner bulk L9 — PE inner-1 Ext A ↩ LLDPE / mLLDPE + slip agent ~16% Heat-seal layer, food-contact surface

↩ = layer fed by the same extruder via die-head flow splitting. Ext E feeds only L5 (EVOH core) — no splitting, dedicated channel. All paired layers (L1/L9, L2/L8, L3/L7, L4/L6) are identical in material because they share one extruder. Thickness % values are indicative references.

Per-Layer Function Reference

Layer Extruder Layer Type Material Primary Function Why It Matters
L1 Ext A PE outer-1 · Surface LDPE · LLDPE + slip / anti-block Print surface, gloss, anti-block Dedicated surface layer — no compromise between appearance and structural strength
L2 Ext B PE outer-2 · Structural LLDPE · mLLDPE (structural grade) Structural strength, stiffness, gauge Independent structural layer — formula optimised for toughness, not surface finish
L3 Ext C TIE Maleic anhydride grafted PE Adhesive bonding — PE-2 to PA Without TIE, PE and PA/EVOH delaminate under stress or retort conditions
L4 Ext D PA Nylon Nylon PA6 · PA6,66 Puncture resistance, protects EVOH outer side PA on both sides of EVOH shields the barrier layer from mechanical damage and moisture
L5 Ext E dedicated EVOH Core EVOH 32–44 mol% ethylene Primary oxygen & aroma barrier Dedicated extruder — never split. Protected by PA + TIE on both sides for consistent barrier quality
L6 Ext D ↩ PA Nylon Nylon PA6 · PA6,66 Puncture resistance, protects EVOH inner side Mirror of L4 — symmetric PA protection on both sides of EVOH core
L7 Ext C ↩ TIE Maleic anhydride grafted PE Adhesive bonding — PA to PE inner-2 Mirror of L3 — maintains bond integrity on the inner side under retort and flex stress
L8 Ext B ↩ PE inner-2 · Structural LLDPE (structural, mirrors L2) Structural strength, flexibility, inner bulk Mirror of L2 — symmetric structural layer ensures balanced film mechanics
L9 Ext A ↩ PE inner-1 · Seal LLDPE · mLLDPE + slip agent Heat-seal layer, food-contact surface Mirror of L1 — dedicated seal layer formula independent of structural requirements

Film Cross-Section — Relative Layer Thickness

Standard Configuration · Symmetric · PE / PE / TIE / PA / EVOH / PA / TIE / PE / PE

L1 · PE outer-1 · Surface
L2 · PE outer-2 · Structural
L3 · TIE
L4 · PA Nylon
L5 · EVOH Core
L6 · PA Nylon
L7 · TIE
L8 · PE inner-2 · Structural
L9 · PE inner-1 · Seal
PE Surface (L1 / L9) PE Structural (L2 / L8) TIE (L3 / L7) PA Nylon (L4 / L6) EVOH Core (L5)

* Thickness ratios are indicative reference values. Actual layer distribution varies by application, EVOH grade and processing parameters. Contact LayerQuestar for application-specific structure recommendations.

LayerQuestar Machinery's 9-layer co-extrusion blown film line produces the PE/PE/TIE/PA/EVOH/PA/TIE/PE/PE structure using 5 extruders with die-head flow splitting — the same proven principle used in the 7-layer symmetric configuration, extended to 9 layers by adding a second PE extruder on each side of the barrier core. The EVOH centre extruder (Ext E) is always dedicated and never split, ensuring consistent barrier layer quality across the full film width. For applications requiring independent material formulas in all 9 layers, a fully asymmetric 9-extruder configuration is available on request.

Technical Specifications

Model Range & Specifications

Reference values under standard operating conditions. Output varies by film width, thickness and material formula. All figures are theoretical reference data — contact LayerQuestar for verified production specifications.

LayerQuestar 9-layer EVOH barrier co-extrusion blown film machine — exterior view showing 5-extruder configuration
Model Film Width (mm) Output (kg/h) † Motor Power (kW) Screw Ø (mm) 9 screws Die Head (mm) Footprint (m)
LQ-9L-1100 Ref. 1,100 150–200 18.5×2 / 15×2 / 11×2 / 7.5×2 / 5.5×1 Φ50/45/40/40/35/40/40/45/50 250 12 × 9.0 × 10.0
LQ-9L-1300 Ref. 1,300 180–250 22×2 / 18.5×2 / 15×2 / 11×2 / 7.5×1 Φ55/50/45/45/40/45/45/50/55 300 13 × 9.5 × 10.5
LQ-9L-1600 Ref. 1,600 250–320 30×2 / 22×2 / 18.5×2 / 15×2 / 11×1 Φ60/55/50/50/45/50/50/55/60 380 14 × 10.0 × 11.0
LQ-9L-1800 Ref. 1,800 300–400 37×2 / 30×2 / 22×2 / 18.5×2 / 15×1 Φ65/60/55/50/50/50/55/60/65 450 15 × 10.5 × 11.5
LQ-9L-2200 Ref. 2,200 380–500 45×2 / 37×2 / 30×2 / 22×2 / 18.5×1 Φ70/65/60/55/50/55/60/65/70 550 16 × 11.0 × 12.0
LQ-9L-2500 Ref. 2,500 450–600 55×2 / 45×2 / 37×2 / 30×2 / 22×1 Φ75/70/65/60/55/60/65/70/75 600 17 × 12.0 × 12.5

† All figures are theoretical reference data. Actual output, power consumption and footprint vary by configuration — contact LayerQuestar for verified specifications. 9-extruder fully asymmetric configurations available on request.

Shared Specifications — All 9-Layer Models

Film Thickness Tolerance ±5%
Temperature Control OMRON PID · ±1°C
Main Motor ABB preferred
Frame 140mm heavy-wall square tube
Gearbox External oil-cooled, 8–10 yr design life
Factory Run Test 72-hour continuous
Control Cabinet Full English labels · 2–3 cooling fans
Standard Configuration 5-extruder symmetric · 9-extruder on request
Buyer Fit

Is a 9-Layer Line Right for You?

A 9-layer EVOH barrier line is the highest-specification blown film investment in the LayerQuestar range. These are the clearest indicators that it is — or is not — the right choice.

Good Fit

  • You produce ambient-stable food packaging requiring shelf life beyond 6 months without refrigeration
  • Your application involves retort processing — the dual-PA structure withstands retort conditions better than a 7-layer structure
  • You need to independently optimise the outer print surface and the structural strength layer — two separate PE layers per side
  • Medical or pharmaceutical packaging with multi-year sterile storage requirements
  • Military, aerospace or precision industrial packaging where maximum barrier and mechanical performance are both required
  • You are currently purchasing 9-layer barrier film from converters and the volume justifies bringing production in-house

Consider a 7-Layer Line Instead If…

  • Your application is standard food vacuum packaging with refrigerated shelf life of 14–30 days — a 7-layer structure covers this fully
  • You do not need to differentiate the surface PE layer from the structural PE layer — a single outer PE layer is sufficient
  • Retort processing is not a requirement
  • Capital investment is a primary constraint — a 7-layer line delivers high barrier performance at meaningfully lower cost
View 7-Layer EVOH Barrier Line

7-Layer vs. 9-Layer — Key Differences

Criterion 7-Layer 9-Layer
Typical structure PE / TIE / PA / EVOH / PA / TIE / PE PE / PE / TIE / PA / EVOH / PA / TIE / PE / PE
PE layers per side 1 (surface + structure combined) 2 (surface and structure independent)
Outer layer formula flexibility Single formula — surface and strength trade-off Two independent formulas — no compromise
Retort suitability Limited — single PE layer less robust under retort Higher — dual PE + dual PA provides better retort resistance
Barrier performance (OTR)* ~0.5–1.5 cc/m²·day (theoretical) ~0.3–1.0 cc/m²·day (theoretical)
Extruder count (standard) 5 (symmetric) or 7 (asymmetric) 5 (symmetric) · 9 available on request
Typical application Vacuum meat, medical, refrigerated food Retort, ambient-stable, long shelf-life, military

* OTR values are theoretical references at 23°C, 0% RH. Actual performance varies by EVOH grade, layer thickness ratio, BUR and processing conditions.

Operator running LayerQuestar 9-layer EVOH barrier blown film line — 5-extruder control panel
Operations

Running a 9-Layer EVOH Barrier Line

A 9-layer line shares the same operational principles as a 7-layer machine but with greater complexity at startup, changeover and shutdown. Plan accordingly before commissioning.

Operator Requirements

  • Minimum 3 operators per shift recommended — 5 extruders running simultaneously requires more monitoring than a 3- or 5-layer line
  • At least one operator must have prior 7-layer or 5-layer EVOH co-extrusion experience
  • EVOH, PA and TIE resin drying protocols must be understood and followed before every startup
  • LayerQuestar provides on-site commissioning support and operator training as standard for all 9-layer installations

Material Handling & Changeover

  • EVOH pre-drying is mandatory — moisture causes bubble instability and permanent barrier degradation
  • PA must be dried to <0.2% moisture content before processing
  • Five separate resin drying systems must be managed simultaneously at startup
  • Shutdown purge sequence is critical — EVOH left in the die head degrades and contaminates subsequent runs
  • Typical structure changeover time: 3–5 hours depending on material combination [NEEDS CLIENT VERIFICATION]

Downstream Compatibility

  • Output film is compatible with standard slitting, rewinding and pouch-making lines
  • For retort applications, film is fed to retort pouch-making lines — confirm retort temperature compatibility with your specific structure
  • Thermoforming and FFS (form-fill-seal) lines are the primary downstream equipment for food applications
  • Corona treatment recommended if film will be printed or laminated downstream
  • Oscillating haul-off available for improved roll geometry on high-speed converting lines
Build Standard

LayerQuestar Build Standard

Five hardware decisions that determine how a 9-layer barrier line performs across a 10-year service life — and how LayerQuestar specifies each one.

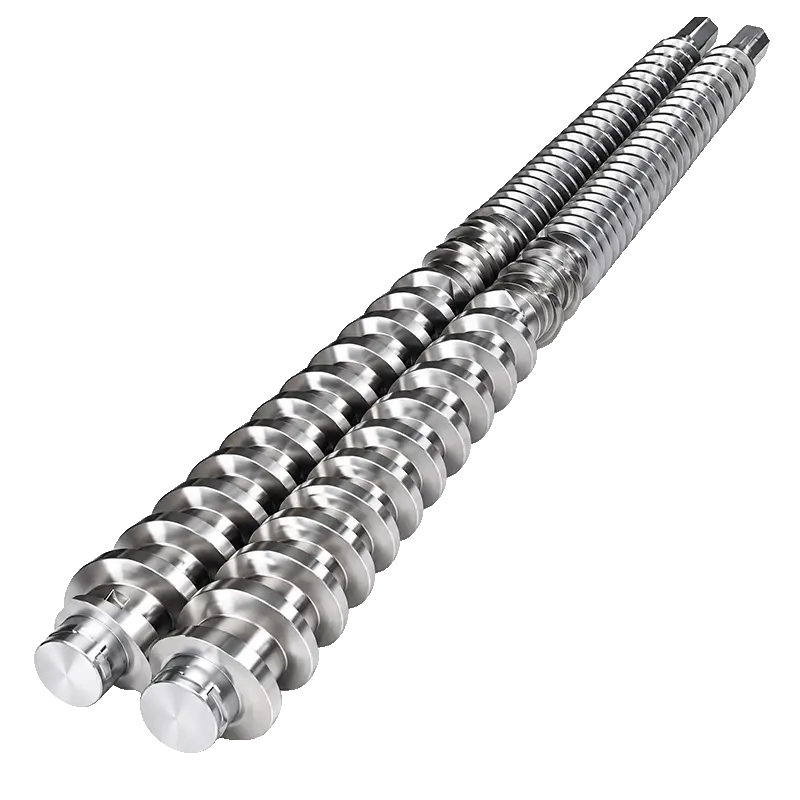
WC bi-metallic screw close-up — LayerQuestar 9-layer EVOH barrier blown film machine
Screw
WC Bi-Metallic

Base: 38CrMoAlA nitrided steel. Overlay: 1.5–3mm tungsten carbide alloy, HRC 59–65. All 5 screws specified identically — handles PA and EVOH processing demands without premature wear. Designed for PCR blends and high-filler masterbatch compounds.

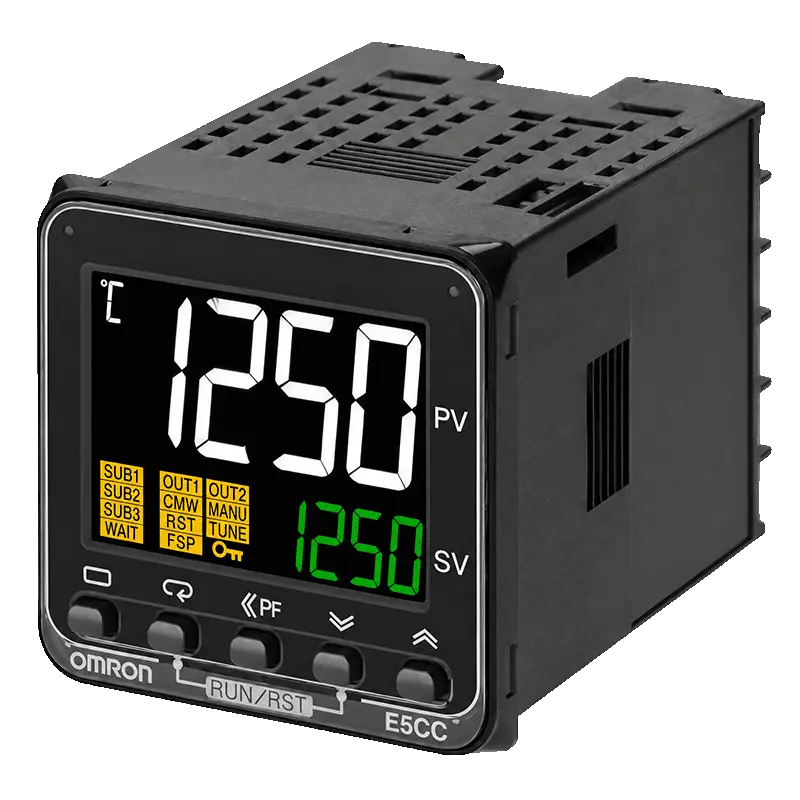
OMRON PID temperature controller close-up — LayerQuestar 9-layer blown film machine
Temperature Control
OMRON PID · ±1°C

OMRON PID controllers on every zone across all 5 extruders and the 9-channel die head. Deviation ±1°C under stable operating conditions. EVOH has the narrowest processing window of any resin on this line — temperature excursions cause irreversible degradation and barrier loss.

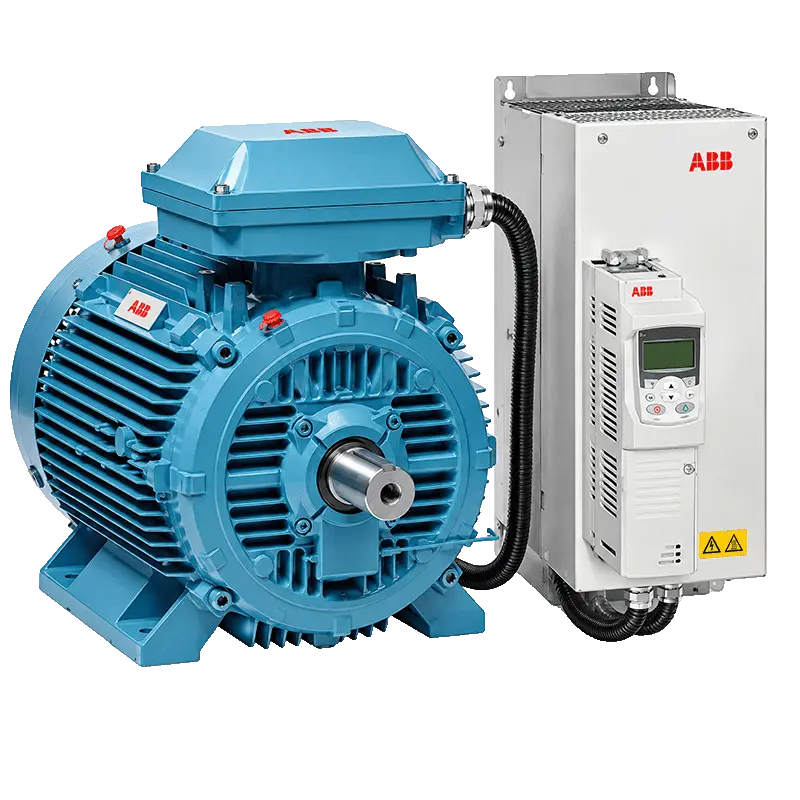
ABB main drive motor close-up — LayerQuestar 9-layer co-extrusion blown film machine
Main Motor
ABB Preferred

ABB specified as standard across all 5 extruder drives. Innomotics and other international-brand motors available on request. VFD-controlled for precise independent speed management per extruder — critical for maintaining layer ratio consistency across 9 layers.

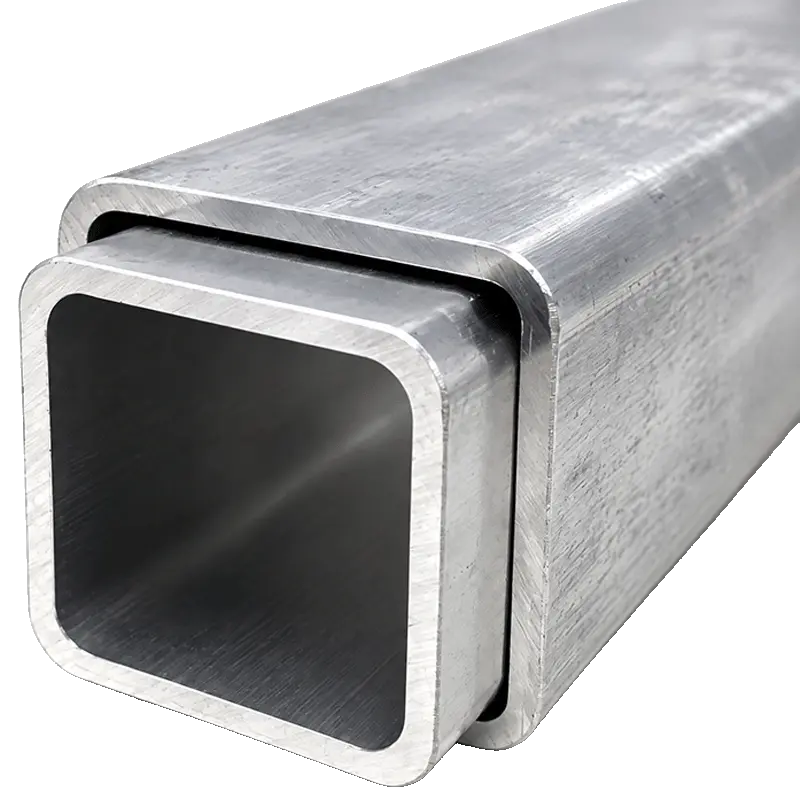
140mm heavy-wall square tube machine frame close-up — LayerQuestar 9-layer blown film machine
Frame
140mm Heavy-Wall Tube

140mm heavy-wall square tube throughout. A 9-layer line carries the greatest extruder mass in the LayerQuestar range — frame rigidity directly affects die-head alignment stability and long-term gauge uniformity across all 9 layers.

External oil-cooled gearbox close-up — LayerQuestar 9-layer blown film machine
Gearbox
External Oil-Cooled

External oil-cooled circulation gearbox on every extruder drive. Designed for 8–10 years continuous service life. Running 5 extruders simultaneously at high output demands sustained thermal stability — internal oil cooling is not specified on any LayerQuestar barrier line.

LayerQuestar factory acceptance test — 72-hour continuous run on 9-layer EVOH barrier blown film machine

72-Hour Factory Acceptance Test

Every LayerQuestar 9-layer line completes a 72-hour continuous factory run test before shipment. The test runs the full 9-layer structure — PE, PE, TIE, PA and EVOH — under production conditions. Film samples are taken at intervals to verify thickness tolerance (±5%), layer distribution consistency across all 9 channels and barrier layer integrity. Test records are provided with every machine.

National High-Tech Enterprise
Certified by the Chinese Ministry of Science and Technology
123+ Patents Granted
Provincial Innovative SME — Zhejiang, China
120+ Countries Served
Established 2008 · Zhejiang, China
After-Sales

Warranty, Spare Parts & Support

A 9-layer barrier line is the highest-value machine in the LayerQuestar range. LayerQuestar's after-sales programme is designed to protect that investment.

Warranty

Standard warranty coverage applies to all major mechanical and electrical components. [NEEDS CLIENT VERIFICATION — confirm warranty period and coverage scope for 9-layer barrier lines]

Wear Parts for 9-Layer Lines

Key wear items include: screw and barrel sets (all 5 extruders), 9-channel die-head lip rings and manifold seals, EVOH-grade screen packs, heater bands and thermocouple sensors. Starter spare parts kit available with every new machine order. [NEEDS CLIENT DATA — confirm kit contents]

Parts Supply

Replacement parts ordered directly from LayerQuestar. Standard parts dispatched within [NEEDS CLIENT DATA — confirm lead time] business days. EVOH-specific components and 9-channel die-head parts held in stock at the Zhejiang facility.

Remote Technical Support

LayerQuestar's engineering team provides remote troubleshooting via video call, email and WhatsApp — covering EVOH processing issues, layer distribution problems, die-head maintenance and startup protocols. On-site commissioning and fault diagnosis visits available. [NEEDS CLIENT DATA — confirm response time commitment]

FAQ

Frequently Asked Questions

Common questions from buyers evaluating a 9-layer EVOH barrier blown film line.

What is the difference between a 9-layer and a 7-layer blown film machine?

The core barrier structure — TIE/PA/EVOH/PA/TIE — is the same in both. The difference is in the PE layers on each side. A 7-layer machine has one PE layer on each side, which must handle both surface performance (printability, gloss, anti-block) and structural strength simultaneously.

A 9-layer machine adds a second PE layer on each side, splitting these functions: the outer PE-1 layer is formulated purely for surface performance, while the PE-2 layer is formulated purely for structural strength and stiffness. The inner side mirrors this. The result is a film where each layer does one job well, rather than two jobs acceptably.

For most food vacuum packaging applications, a 7-layer structure is sufficient. The 9-layer structure is specified when retort processing, ultra-long ambient shelf life, or independent surface and structural layer optimisation are genuine requirements.

Why does a 9-layer machine only need 5 extruders?

The 9-layer structure PE/PE/TIE/PA/EVOH/PA/TIE/PE/PE is fully symmetric. Every layer has an identical mirror layer on the other side of the EVOH core: L1 mirrors L9, L2 mirrors L8, L3 mirrors L7, L4 mirrors L6. Only L5 (EVOH) has no mirror.

Because each pair of mirrored layers is identical in material, one extruder can feed both layers simultaneously via die-head flow splitting. Extruder A feeds L1 and L9, Extruder B feeds L2 and L8, Extruder C feeds L3 and L7, Extruder D feeds L4 and L6. Extruder E feeds only L5 (EVOH) — dedicated, never split. Five extruders produce nine layers.

Is a 9-extruder fully asymmetric configuration available?

Yes — a fully independent 9-extruder configuration is available on request, where each of the 9 layers has its own dedicated extruder and can carry a completely different material formula. This enables full asymmetric design: for example, the outer PE-1 surface layer can carry a white masterbatch and UV stabiliser package, while the inner PE-1 seal layer carries a specific anti-fog and slip additive package — with no compromise between the two.

For most applications, the standard 5-extruder symmetric configuration is sufficient. The 9-extruder configuration is a custom order — contact LayerQuestar to discuss your specific requirements.

Is a 9-layer line suitable for retort packaging?

The 9-layer PE/PE/TIE/PA/EVOH/PA/TIE/PE/PE structure is better suited to retort applications than a 7-layer structure, primarily because the dual PE layers provide greater structural integrity under the thermal and pressure stress of retort processing, and the dual PA layers provide stronger protection for the EVOH core against moisture absorption during the retort cycle.

However, retort packaging involves specific material grade requirements — not all PE, PA or EVOH grades are retort-rated. Contact LayerQuestar with your retort temperature, processing time and shelf-life requirements for a specific structure and material grade recommendation.

What oxygen transmission rate can a 9-layer EVOH film achieve?

As a theoretical reference, a PE/PE/TIE/PA/EVOH/PA/TIE/PE/PE structure with approximately 9% EVOH layer thickness can achieve an OTR in the range of 0.3–1.0 cc/m²·day at 23°C, 0% RH — marginally better than a 7-layer structure at equivalent EVOH thickness, primarily because the dual PA layers provide better moisture protection for the EVOH core, which preserves barrier performance under humid conditions.

Actual barrier performance depends on EVOH grade, layer thickness ratio, BUR, processing conditions and end-use humidity environment. Contact LayerQuestar with your specific application for guidance.

How does running cost compare to a 7-layer line?

The capital cost of a 9-layer line is higher than a 7-layer line, primarily due to the more complex 9-channel die head and the larger machine footprint. The extruder count is the same (5 extruders), so the motor and drive cost difference is smaller than it might appear.

On running costs, the dominant variable is resin cost. A 9-layer structure uses more PA than a 7-layer structure (two PA layers vs. two PA layers at similar thickness — comparable), but the additional PE-2 structural layers add PE resin cost. In practice, the total resin cost per kilogram of film is similar to a 7-layer structure of equivalent total gauge. Contact LayerQuestar for a detailed cost-per-kilogram analysis based on your specific structure and output requirements.

Can the 9-layer line run as a 7-layer or 5-layer machine?

The machine can be operated with selected extruders purged and channels substituted, effectively producing a reduced-layer structure on the 9-layer platform. This gives the line flexibility to serve multiple product families from a single machine.

However, a 9-layer line is optimised and priced for 9-layer barrier film production. If your primary application does not require the full 9-layer structure, a 7-layer or 5-layer line will deliver better value. Contact LayerQuestar to discuss the right configuration for your product mix. [NEEDS CLIENT VERIFICATION — confirm partial-layer operating mode support for 9-layer platform]

How long does installation and commissioning take?

Commissioning a 9-layer line is the most complex installation in the LayerQuestar range, due to the 9-channel die-head alignment requirements, the number of resin drying systems to qualify, and the EVOH processing validation. Typical commissioning duration is [NEEDS CLIENT VERIFICATION — confirm standard commissioning timeline for 9-layer lines].

LayerQuestar provides on-site commissioning engineers as standard. The commissioning scope includes mechanical installation verification, electrical and control system check, initial film run with all 9 layers, layer distribution verification and operator training on EVOH and PA handling protocols.

Get Started

Ready to Specify Your
9-Layer Barrier Line?

Tell LayerQuestar your target film structure, output requirement and application — we will recommend the right configuration (5-extruder symmetric or 9-extruder fully asymmetric on request) and provide a detailed proposal.

From Recycling to Finished Bags — One Supplier. One Line. One Responsibility.